Lean, Six Sigma, Theory of Constraints and the Mountain:

Matterhorn_Riffelsee_2005-06-11 - Copy.jpg

Recently there have been a lot of discussions about which is best – Lean, Six Sigma or Theory of Constraints? Is Lean Six Sigma better than Lean or Six Sigma?

In this brief post, I will try to view this question from my viewpoint. There is a saying based on the 9th century Zen Buddhist teacher Qingyuan Weixin which I have paraphrased loosely below;

“At first I saw the mountain as a mountain. Then when I learned more and more, I realized that the mountain is not a mountain. But now that I have learned it even more, I see that the mountain is a mountain again.”

If you change the term mountain with “Lean” and “a set of tools”, we can paraphrase it as follows;

“At first I saw Lean as a set of tools. Then I learned more and more, I realized that Lean is not a set of tools. But now that I have learned it even more, I see Lean as a set of tools again.”

You can change Lean to any other philosophy in the above saying. I was taken aback by the saying when I first read it. But gradually it made more sense.

When we first learn about Lean, you hear about the tools. You perceive it as a solid and fixed set of tools. This could include 5S, SMED, Poka Yoke, VSM etc. This kind of categorization and labeling makes us believe that Lean is a set of tools and something that is static. It makes us feel that we know it.

Lean = 5S + SMED + Poka-yoke + VSM +…….

Once we learn more and more, we come to realize that it is not static but dynamic. There is no “one size fits all” solution. There is no magic bullet. The strategy that worked for one company does not work for the other. Then we start to see Lean as not a set of tools.

Lean = Eliminate Waste

However, once we learn more and more, and start applying Lean, we gain a new awareness. We realize that Lean has an overall form and yet is free flowing. You realize that you need to understand the problem first, and then address the problem using the appropriate tool. You become spontaneous and you just know which tool to use when and how. Now, Lean has become a set of tools again.

Lean = Understand the context of the problem, and address the problem using the right tool

Always keep on learning…

In case you missed it, my last post was Chewbacca, Poka-Yoke and Respect for People.

Chewbacca, Poka-Yoke and Respect for People:

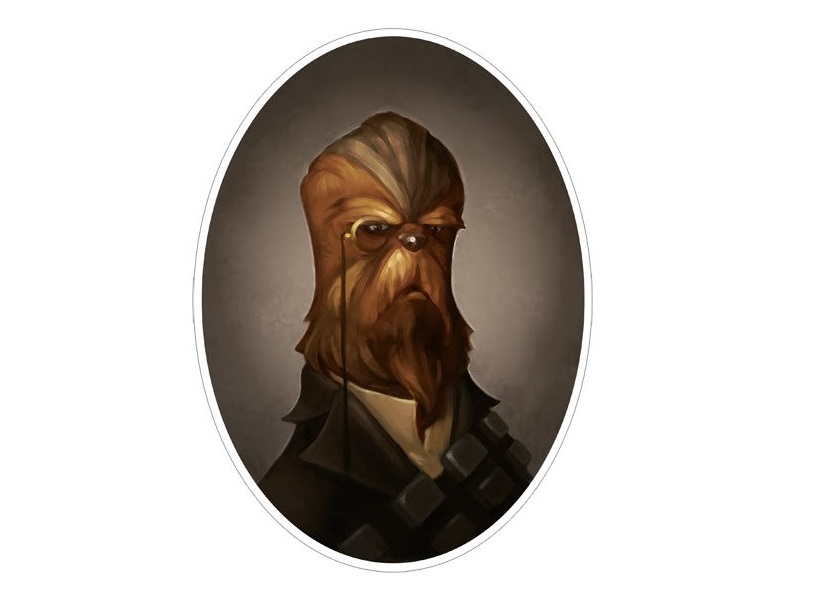
Sir Chewbacca

One of key concepts in Toyota Production System with respect to Quality (other than Jidoka/Autonomation) is Poka-Yoke (ポカヨケ), or Error Proofing. “Yokeru” in Japanese means “to avoid”. “Poka” means “error” or “blunder”. The story behind Poka-Yoke has an underlying theme of respect for people.

Baka to Poka:

The concept of Poka-Yoke was made famous by Shigeo Shingo, perhaps one of the best Industrial Engineers. He coined it as “Baka-Yoke”. “Baka” in Japanese means “idiot” or “fool”. Thus, Baka-Yoke means “fool proof”.

Around 1963, Arakawa Auto Body adopted a fool proofing device as part of a Baka-Yoke program. This device prevented seat parts from being spot welded backwards. The story goes that one of the part–time workers started crying when the supervisor explained about the fool-proofing device because the workers were sometimes mixing up left and right handed parts.

“Have I really been such a fool”, she asked. She ended up staying home that day. The supervisor had to go to her home to convince her to come back by explaining that she is not a fool. The device was being used because anybody can make inadvertent mistakes.

Shingo was told this story, and after some thought he changed the name to “Poka-Yoke”. Thus choosing a term that communicates more respect for the worker.

Poka-Yoke and Respect for People (RFP):

The story above shows that Shingo was being respectful and the new name of Poka-Yoke is certainly more meaningful since it does not put any blame on the employee. I have heard this story being used to explain Respect for People. But more than the story, I feel that the concept of Poka-Yoke is a part of Respect for People. You may have heard that things go wrong sometimes, especially when the operator is doing a highly repetitive activity. The big red book of Poka-Yoke by Nikkan Kogyo Shimbun states the following;

The idea behind Poka-Yoke is to respect the intelligence of the workers. By taking over repetitive tasks or actions that depend on vigilance or memory, Poka-Yoke can free a worker’s time and mind to pursue more creative and value-adding activities.

Extrinsic and Intrinsic Respect for People:

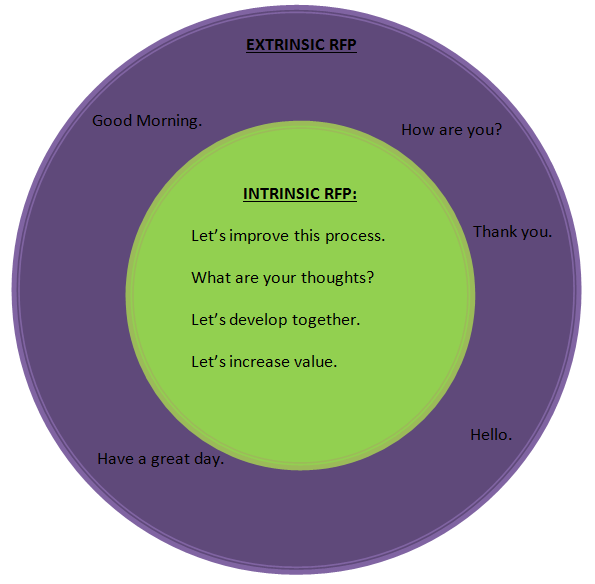
The more I read about TPS and Respect for People, I am coming to view Respect for People as Extrinsic and Intrinsic RFPs.

extrinsic and intrinsic

The Extrinsic RFP is superficial in nature. This is the basic respect you give to your fellow human beings. This is you being nice to people, the basic manners!

The Intrinsic RFP is the meat and potatoes or the true essence of Respect for People. As a leader in your organization you ensure that the work performed by an employee is value added. As the leader of your organization, it should be your job to develop your employees and ensure that they remain valuable assets. Toyota says that they believe in making people before making cars. Respect for people means that the organization is providing an environment where the employees are doing only value added activities.

How does one increase the worth of an employee? You can increase their worth by developing the employee to understand the value in his work. You can increase the worth by training him to look for gaps between the ideal state and current state. By understanding this gap, you can further develop him to take countermeasures and corrective actions to move closer to the ideal state. Ideally, the employee would now be able to train the employees underneath him. The employee is now at a stage to be making decisions and implementing the improvements on his own. In other words, he is empowered.

You might wonder whether Respect for People is value added. The traditional notion of value added activity is that the activity is something that the customer is willing to pay for. My view is that by creating the equation making things is making people, Toyota has transformed people development as a value added activity.

Chewbacca’s Connection to Baka:

I came across an article that suggested that maybe George Lucas created the name Chewbacca from the Japanese phrase “Chū baka” which means “Medium Stupid/Fool” or “Average Idiot”. There is of course no conclusive evidence for this. George has admitted that he was influenced by Japanese culture and movies while making Star Wars. I thought this was a nice story with relation to Poka-Yoke and Respect for People. Let Chewbacca remind you the need for Poka-Yoke as opposed to Baka-Yoke, and Respect for People.

Always keep on learning…

Image Credit – Sir Chewbacca (mcfeezy )

In case you missed it, my last post was “Would Ohno Change the term ‘Lean’”.

Would Ohno Change the Term “Lean”?

vlcsnap-2016-01-10-15h31m11s593

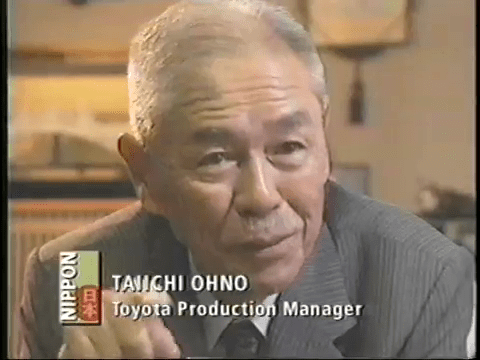
Taiichi Ohno is the father of Toyota Production System. Lean Manufacturing is based on Toyota Production System. The term “Lean” was coined by John Krafcik in his MIT Sloan 1988 Fall paper “Triumph of the Lean Production System”. His terminology was “Lean Production” or simply “Lean”. He noted that;

“Plants operating with a “lean” production policy are able to manufacture a wide range of models, yet maintain high levels of quality and productivity”.

There have been many discussions about whether “Lean” is the correct terminology or not. Lean is supposed to have a negative connotation with it. There is a tendency to assume that Lean indicates reduction – reduction in inventory, reduction in cycle time, reduction in costs etc.

I was pleasantly surprised when I came across Taiichi Ohno’s thoughts on “Lean” Management. As indicated in my last post, Ohno started a consultancy group soon after leaving Toyota. This group was called the New Production System Research Association. Isao Shinohara wrote a book on this called “New Production System – JIT Crossing Industry Boundaries”, in 1985. The main theme of this book is that the TPS ideas are applicable across multiple industries. This book also had a section with an interview with Taiichi Ohno.

Limited, Not Leaner, Management:

In Ohno’s words;

“The idea is to produce only what can be sold and no more. The idea is to limit, not necessarily to reduce, the quantity. The important thing is to keep production costs low whle limiting the production level. It is meaningless to say that producing 15,000 units will reduce production costs when you can only sell 10,000 units.”

He continues;

“The essence of limited management (genryo keiei) and limited production (genryo seisan) is to produce what can be sold at the lowest possible cost.”

My favorite section of the interview was when Ohno was asked about reducing or eliminating inventory.

“Shinohara – Many people think that Toyota Production System is a method for reducing inventory or eliminating inventory altogether.

Ohno – That is not right. I’ve said this so many times, but people don’t seem to understand. The Toyota production system is a philosophy of changing the production and management flows.”

Analogy of a Boxer:

boxer

Taiichi Ohno compares limited production to the regimen of a boxer in his book “Workplace Management”. The boxer has to be in a specific weight classification. If he misses a few training sessions and he puts on weight, he can no longer compete in his class. He would then have to diet to slim down and maintain his weight. This is akin to a company trying to reduce inventory. If he loses more than his intended weight, he will run out of energy and lose the fight. This sort of slimming down is undesirable. Ohno advises against going on a diet for a company without thorough understanding. He calls it a dangerous idea to trim down so much that the essential meat of the company is cut into.

Always keep on learning…

In case you missed it, my last post was “Don’t Strive for Perfection – 60% is good enough”.

60% is Good Enough

AN00222094_001_m

It is 2016! It is a new year and it is time for New Year’s resolutions.

I have been thinking about what I should write for New Year’s. I wanted this post to be something personal.

Pursuit of Rationality:

I came across the phrase “Pursuit of Rationality” in “Toyota Production System – First Textbook”, an internal document at Toyota from the 1970’s. The loose English translation of the relevant section is given below;

“Through thorough observation and pursuit of rationality, we can lay the strong foundation upon which we can build the strong castle of improvement”.

My interest piqued at the phrase “pursuit of rationality”. This has a strong resemblance to “pursuit of excellence or perfection”. It is explained in Taiichi Ohno’s book, Toyota Production System – Beyond Large Scale Production, that rationalization in Japanese writings indicate activities undertaken to upgrade technology, improve quality, and reduce costs. Being rational is being value adding, and not producing waste.

My message to myself and to the readers of my blog is also about pursuit – the pursuit of excellence while pursuing rationality. This may be better explained in Ohno’s thought process as well. Soon after leaving Toyota, Ohno founded the New Production System Research Association, a consulting group with his friends. This group had 25 doctrines that they also pursued. I am focusing on one of these for this New Year!

 Don’t seek perfection. 60 percent is good enough!

We spend a lot of time sharpening our axes, and never strike the tree. We try to get everything just perfect to start doing something, write a post, write a book, start coding etc. We wait and wait, and we end up never doing what we wanted. So let’s pursue rationality this year, and take action. We can always make it better, once we have started it. Let’s plan a little and then DO a little.

Step by Step:

The following is a story I heard from India.

It was pitch dark, and a man had to go to the next town miles away. All he had was a small lantern, and this could light only a few steps in front of him. The man just stood there not knowing what to do. The journey seemed so long and the night seemed very dark. He became sad and depressed.

A monk saw the man standing in front of his house, and asked the man what he was doing.

“I have to go to the next town, and I am packed for the trip. I do not know what to do. The journey seems long, and the night seems dark,” the man responded. “All I have is this small lantern.”

“You do not need a big lamp to illuminate the whole way,” the monk explained. “As you move, the light will move in front of you so that the next few steps are always clear. All you need to do is to hold on to this light and start walking. As the darkness clears with the rising of the sun, if you keep walking you will reach your destination”.

Always keep on learning…

I wish all my readers a prosperous and a rational 2016!

In case you missed it, my last post was about “The Rashomon Effect at the Gemba.”

The Rashomon Effect at the Gemba

R

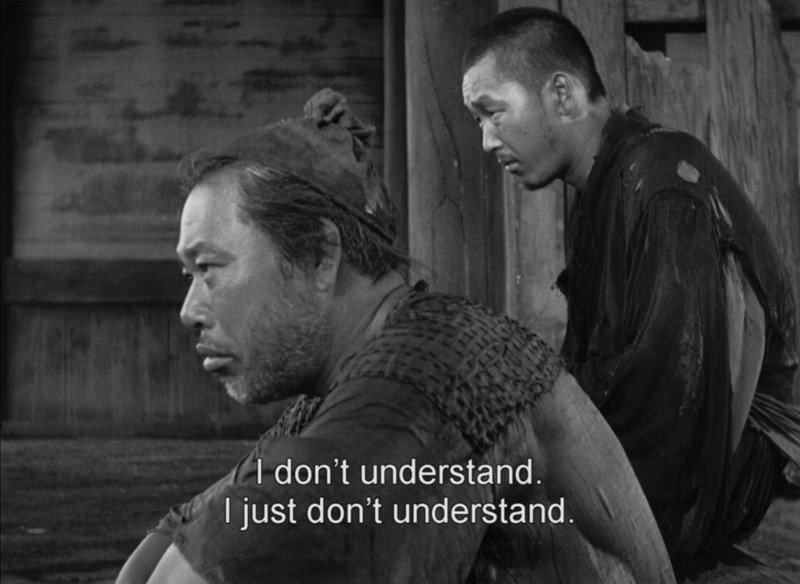
“Rashomon” is a classic Akiro Kurosawa film, based on the story “In a Grove” by Ryūnosuke Akutagawa. In the movie, the same series of events are described by four people from different backgrounds. Each version of the story varies differently than the others. All of the four characters saw and experienced the same events, yet they all tell different versions of how things unfolded and who did what. This has come to be called as “Rashomon Effect” in pop culture. The opening line of the movie is “I don’t understand. I just don’t understand”, and this lays the groundwork of the whole movie.

This type of “Rashomon Effect” can also happen at the gemba. One of the great stories about Taiichi Ohno, the father of Toyota Production System, is about the Ohno Circle. The story goes that Taiichi Ohno would take the Engineer or the supervisor to the floor, and if Ohno feels that the supervisor does not see what he sees or that the supervisor does not understand his viewpoint, he would draw a circle on the production floor and ask the supervisor to stand inside it. The supervisor has to stand inside the circle until he starts to see the operational wastes. Then his job is to immediately fix the problems. Ohno is seeing all the waste and problems on the floor. The same activity is also being seen by the engineer. He does not see any of the wastes that Ohno sees. Ohno is said to have been short tempered with this and would scold the engineers. Ohno would return to the floor sometimes 6-8 hours later and would ask what they saw after standing in the circle.

ohno

As I was reading through “Toyota Production System (Kanban) Book”, an internal Toyota document from 1970’s, I came across a paragraph about the Ohno Circle. The rough translation is as follows;

It is expected that the supervisors were scolded by Ohno on the floor. Ohno would make them stand on the floor by drawing a circle. This is similar to being scolded by teacher at school as in “go stand in the hallway!” At school, the purpose is quite different, which is to exclude the student from the classroom. On the floor, the supervisor has to see the problem and improve it. This problem can come into view only by continuous observation in that position, inside the circle.

“Why, why, why, why, why”, ask why five times. This is therefore referred to as the observation method.

I enjoyed that the document tries to differentiate between standing in the hallway and standing on the production floor.

The Ohno Circle exercise is just that – an exercise to strengthen your waste sensors. The more you look, the more you observe. The more you observe, the more you become aware of things differently. Why are there three bins of components on the table? Why does the operator spend time picking the “right” component for assembly? Why does the operator check the component 4-5 times? And so on. Pretty soon the Rashomon effect erodes away. Now the waste becomes visible. Once the waste is identified, then Ohno instructs to ask why again and again, until the root cause can be identified and the issue is fixed.

Bicycle Riders – a Zen Story:

The Rashomon effect reminds me of a Zen story I heard:

A Zen Teacher saw five of his students return from the market, riding their bicycles. When they had dismounted, the teacher asked the students,

“Why are you riding your bicycles?”

The first student replied, “The bicycle is carrying this sack of potatoes. I am glad that I do not have to carry them on my back!”

The teacher praised the student, saying, “You are a smart boy. When you grow old, you will not walk hunched over, as I do.”

The second student replied, “I love to watch the trees and fields pass by as I roll down the path.”

The teacher commended the student, “Your eyes are open and you see the world.”

The third student replied, “When I ride my bicycle, I am content to chant.”

The teacher gave praise to the third student, “Your mind will roll with the ease of a newly tuned wheel.”

The fourth student answered, “Riding my bicycle, I live in harmony with all beings.”

The teacher was pleased and said, “You are riding on the golden path of non-harming.”

The fifth student replied, “I ride my bicycle to ride my bicycle.”

The teacher went and sat at the feet of the fifth student, and said, “I am your disciple”.

Always keep on learning…

In case you missed it, my last post was about “Brooks’ Law – Mythical Man Month”.

Brooks’ law – Mythical Man-Month

mitico_cap1_1

I recently finished reading the book “The Mythical Man-Month”. This book was written by Frederick Brooks Jr. and first published in 1975. This book has been quoted as “the Bible of Software Engineering.” It is based on the experiences of the author at IBM while managing the development of OS/360.

Although the topic of the book is software engineering, I believe that the principles identified in the book are applicable to any project.

The main idea of the book is about the mythical man-month which may be intuitive to some people. This basically can be explained as follows;

  • Project cost is proportional to the number of people involved. Cost = number of men * number of months.
  • Project progress is not proportional to the number of people involved. Number of men or people and months are not interchangeable.

Brooks says “Man-month as a unit for measuring the size of the job is a dangerous and deceptive myth.”

This book also gave us Brook’s law. Brook’s law can be stated as follows;

“Adding manpower to a late software project makes it later.”

There is some resemblance to Braess’ paradox in traffic networks, which can be loosely stated as “Adding extra capacity to a network in some cases brings down the overall performance of the network”. I will discuss more about Braess’ paradox at a later time.

Brooks’ Law:

There are multiple factors that make Brook’s law work. The first is the amount of time needed for a new member to get accustomed to the project. This is treated as “ramp-up” time. The second factor is communication. As more members are added to a team, the complexity of communication requirements increases. This is referred to as communication overhead. The third factor is the project type. If there are sequential tasks that are independent in nature, this results in delays due to the first two factors. When a task cannot be partitioned because of sequential constraints, the application of more effort has no effect on the schedule. In Brooks’ words; “The bearing of a child takes nine months, no matter how many women are assigned.”

Why Did the Tower of Babel Fall?

This is perhaps the section that I enjoyed the most. Brooks performs a “management audit” on the Babel project. The tower of Babel is a famous story in Bible, in the book of Genesis. The people of the world wanted to build a tower that reached to the heavens. In the story, the people spoke only one language, and God made the people speak in different languages so that they could not understand each other, and the tower was never completed.

Brooks reviewed the following factors for the “Babel Project”;

A clear mission: There was a clear mission – to build the tower.

Manpower: There was plenty of manpower.

Materials: Clay and asphalt were abundant.

Time: There was no time constraint noted in the story.

Technology: The technology available at that time was adequate.

The Tower of Babel was never built because of two reasons – communication and organization. Brooks explains that lack of effective communication led to lack of coordination. When coordination failed, the project came to a halt. In today’s world, lack of effective communication is very relevant. In my view, the point of organization is about system optimization. Pursuit of local optimization will always result in a decrease of system performance.

I highly encourage the reader to read the Mythical Man-Month book. The first edition is available electronically here.

Funny Project Management Story:

I will end with a story I heard about project management.

A man is flying in a hot air balloon and realizes he is lost. He reduces height and spots a man down below. He lowers the balloon further and shouts:

“Excuse me, can you help me? I promised my friend, I would meet him half an hour ago, but I don’t know where I am.”

The man below says, “Yes, you are in a hot air balloon, hovering approximately 30 feet above this field. You are between 40 and 42 degrees North latitude, and between 58 and 60 degrees West longitude.”

“You must be an Engineer,” says the balloonist.

“I am,” replies the man. “How did you know?”

“Well,” says the balloonist, “everything you have told me is technically correct, but I have no idea what to make of your information, and the fact is I am still lost.”

The man below says, “You must be a project manager”

“I am,” replies the balloonist, “but how did you know?”

“Well,” says the man, “you don’t know where you are or where you are going. You have made a promise which you have no idea how to keep, and you expect me to solve your problem. The fact is you are in the exact same position you were in before we met, but now it is somehow my fault.”

Always keep on learning…

In case you missed it, my last post was about “The Mystery of Missing Advent Calendar Chocolates”.
The Mystery of Missing Advent Calendar Chocolates:

advent

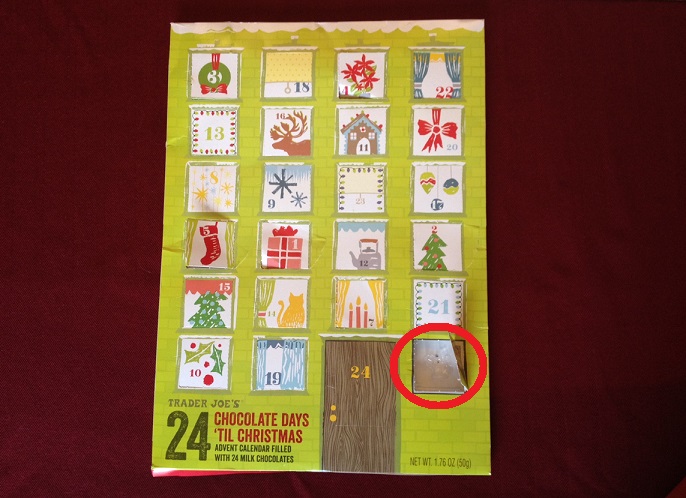
It is Christmas time, which means it is advent calendar time for the kids and for those of us who are kids at heart. My wife bought our kids chocolate advent calendars from Trader Joe’s. For those who do not know advent calendars, these are countdown calendars to Christmas starting on December 1st. Each day has a window which you can open to reveal a chocolate. Each day has a uniquely shaped chocolate, a Christmas tree, a stocking etc. The kids love this.

We keep the advent calendars on the top of our refrigerator to ensure they are not tempted to eat all of the chocolate at once. This morning, I found the advent calendars on the table and a crying Annie. Annie is our youngest daughter. She was very upset.

“I did not get any chocolate today from my calendar”, she said while crying.

“You must have eaten it already”, was my response. Of course, the kids eat chocolate and sometimes they are impatient and eat more than one day’s worth. In my mind, it was a reasonable assumption to make.

Annie explained that she opened the window with 6 on it and did not find any chocolate. I looked at the calendar, and sure enough, the window for day 6 on it was open. My initial hypothesis stayed the same – Annie ate the chocolate, and she is not telling me the entire truth.

My wife suggested she open the window for day 7 and eat that chocolate. Annie then proceeded to open the window with 7 on it, in front of me. Lo and behold, it did not have any chocolate. Annie looked at me with sad eyes. I realized, I was wrong to have assumed that Annie had eaten the chocolate!

“This is a mystery”, said Audrey, her twin sister.

Now I had a second hypothesis – those darn calendar makers; they do not know what they are doing. They obviously missed filling all the spots with chocolate. As a Quality Engineer, I have seen operator errors. I have now jumped to my second hypothesis.

Having thought about for a bit, I looked at the available information. Based on what Annie told me, the chocolate was not in its spot for two consecutive days. These calendars did not have the numbers in the consecutive order. They were placed in random order. It did not strike to me that two candies at different locations would be missing candy. She had opened a spot between 6 and 7 on an earlier day, and it had the candy.

I had a reasonable hypothesis – the operator/equipment missed the spots in the calendar. I have seen it happen before in different environments. But still, something was not right.

I proceeded to put the advent calendar back onto the top of the refrigerator. Then I thought of something. I wanted to test the calendar more. I carefully opened the calendar from the base. It was a card board box with a plastic tray inside.

Just then I found out what happened! On multiple places, the chocolate was missing. The chocolate were misplaced from its cavities. They were all gathered at the bottom of the box. It could be from the transportation. It could be the end user i.e. my excited young daughter who shook the calendar. It could be the design of the calendar that allows extra space between the tray and the cardboard.

The most important thing was that Annie was now happy that she got her candies. Audrey was happy that we indeed had a mystery that we could solve. My wife and I were happy that our kids were happy.

Final Words:

This personal story has made me realize again that we should not jump to conclusions. Listen to that tiny little voice that says “there is something more to this”…

Always keep on learning…

In case you missed it, my last post was about “Lady Tasting Tea”.

Let’s Talk About Tea:

wonderland

This week, I was talking to one of my colleagues and going off on a tangent we began discussing tea. His parents are from UK. Today’s post is inspired by that conversation.

Milk First or Tea First:

The question of whether to add milk first or tea first is an interesting one. As part of writing this post, I did some research on this one. The first documented account of milk being added to tea is from Johan Nieuhof (1618-1672), a steward of the then Dutch ambassador to China. He wrote about adding one fourth of warm milk to tea with salt. The idea of using milk with tea was made popular in Europe by social critic Marie de Rabutin Chantal, the Marquise de Seven in 1680.

The socially correct protocol, according to Douglas Adams (author of Hitchhiker’s Guide to the Galaxy) and many others is to add milk in after tea. There are many anecdotes on why this is the case. The most popular version is about the quality of tea cups back in the day. Pouring hot tea first broke the low quality cups. The upper class of the society showed off their high quality cups by pouring hot tea first and then milk. The people who could not afford high quality tea cups poured milk first and then tea. Another reason could be also the way the process of making tea was documented. As noted above, the documented process was to add milk to tea.

George Orwell even wrote an essay on making tea called “A Nice Cup of Tea”. His preference was to add tea first and then milk. His logic was as follows;

One should pour tea into the cup first. This is one of the most controversial points of all; indeed in every family in Britain there are probably two schools of thought on the subject. The milk-first school can bring forward some fairly strong arguments, but I maintain that my own argument is unanswerable. This is that, by putting the tea in first and stirring as one pours, one can exactly regulate the amount of milk whereas one is liable to put in too much milk if one does it the other way round.

Douglas Adams on the other hand liked to add milk first even though it was not the socially correct protocol. Today, scientists will tell you that the proper way of making tea is to add the milk first and then tea. Milk proteins when exposed to a temperature above 75 degrees C (167 degrees F) will start to degrade through the process of denaturation. This is more prone to happen when milk is added to tea rather than when tea is added to milk.

The Lady Tasting Tea:

The story of the lady tasting tea is perhaps the most fantastic story in the field of statistics. There are a few different versions as to where the incident took place. The story goes that in an English afternoon in 1920’s, a statistician, a chemist and an algologist were sitting together. The statistician offered to make tea, and proceeded to pour tea and then milk. The algologist, a lady (hence the name a lady tasting tea) objected to the process. She told the statistician that she preferred to have the milk poured before tea. She claimed that she could tell the difference. The chemist who was the fiancée of the algologist immediately wanted to test her claim, as any warm blooded scientist would do. The statistician proceeded to create an impromptu test for the lady. He created four cups of tea with milk first, and then four cups of tea with tea first. He randomized the cups using a published collection of random sampling numbers. The lady was informed of the test protocol and then she tasted each cup and identified all the cups accurately, thus standing by her claim.

The statistician was Sir Ronald Fisher, the chemist was Dr. William A Roach and the lady algologist was Dr. Blanche Muriel Bristol. The story was documented by Sir Fisher in the groundbreaking book “The Design of Experiments” and in his paper “The Mathematics of a Lady Tasting Tea”. The probability of the lady getting all the results correct was 1/70 = 0.014. This value is less than the magical 0.05. Interestingly, Sir Fisher wrote the following about the 0.05 value in the paper;

“It is usual and convenient for experimenters to take 5 percent, as a standard level of significance…”

If the lady had gotten one result incorrect, the p-value would had been 0.243, and the testers would have failed to reject the null hypothesis that the lady has no ability to tell the difference between the two styles of making tea. Thus, one can say the test is not fair since if the lady failed once, it would not help justify her claim. In the paper, Sir Fisher advised that to improve the test, one should use 6 cups each of tea. The p-value of getting one incorrect is only 0.04, which is still less than 0.05. Thus, the lady has a little more leeway.

This story helped explain the idea of randomization and significance testing. The test’s efficacy is improved further if the total number of particular styles were kept secret. Dr. Bristol was told about the exact number of each style of tea beforehand.

The Answer to the Ultimate Question of Life, the Universe, and Everything:

In Hitchhiker’s Guide to Galaxy, the answer to the Ultimate Question of life, the universe and everything is given as 42! I came across a possible explanation during my research for this post based on Douglas Adam’s passion for tea.

42 = fortytwo

For tea two.

Two for tea!

Always keep on learning…

In case you missed it, my last post was about Respect for Humanity.

Respect for Humanity (An early theme in Toyota Production System):

people1

This post is mainly about Respect for People in Toyota Production System, to show that this idea has been an integral part of Toyota Production System from the early days on.

“Toyota Production System – The foundation is respect for human rights”.

This is a quotation from a Toyota Production System book. Respect for people got famous with the famous Toyota Way document in 2001. This principle has been included within Toyota Production System for a long a time. In fact, the quotation I have cited is from “Toyota Production System First Textbook”. This is one of the early documents created within Toyota in the early 1970’s. An interesting trivia is that some of the text was written by Fujio Cho, the very person behind the Toyota Way 2001 document.

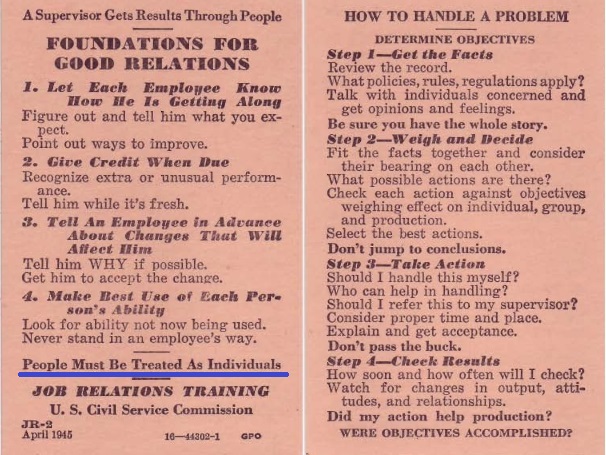
Section 5 of this document is titled “Man-Hour Reduction and Human Relations”. This section calls out TWI (Training Within Industry) Job Relations manual and cites “People must be treated as individuals” phrase from the Job Relations manual.

JR

I have written about TWI previously here. TWI was an emergency service by US to help nation’s war contractors and essential production. There was a need to produce a lot in a short amount of time, and this required training operators to be better within a short amount of time. C R Dooley, the Director of TWI, stated the following; “TWI’s objectives were to help contractors to get out better war production faster, so that the war might be shortened, and to help industry to lower the cost of war materials.” Job Relations is one of the manuals of the TWI program. In the foreword of this manual, C R Dooley stated that “Giving workers technical skill alone is not enough. Supervisors must give every man and woman at work the leadership that enlists cooperation and teamwork.” Toyota added Job Relations to its internal training curriculum in 1951.

The “Toyota Way 2001” document made “Respect for People” the new thing in lean. This theme was not at all present in any of the western books on Lean or Toyota Production System. Naturally, this theme got a lot of attention fast.

Yasuhiro Monden’s Write-up on Respect for Humanity:

Respect for people also goes by Respect for Humanity. In my opinion, this was best described by Prof. Yasuhiro Monden in his 1983 book “Toyota Production System”. He wrote;

“At Toyota, respect for humanity is a matter of allying human energy with meaningful, effective operations by abolishing wasteful operations. If a worker feels that his job is important and his work significant, his morale will be high; if he sees that his time is wasted on insignificant jobs, his morale will suffer as well as his work.”

Prof. Monden also links to the ability of the worker to stop the line in case of a problem with Respect for Humanity. He states “Since quality control based on autonomation (Jidoka) calls immediate attention to defects or problems in the production process, it stimulates improvement activities and thus increases respect for humanity.”

Prof. Monden also gives two rules to follow when making job improvements;

  • Give the worker valuable jobs – the job performed by the worker (operator) should not be riddled with non-value added activities.
  • Keep the lines of communication within the organization open – A relationship of trust and credibility needed for improvement activities need open lines of communication.

One of the mantras at Toyota is “Monozukuri wa hitozukuri” or “Developing products is about developing people”. This idea is underlined by Prof Monden. He has identified three sub-goals for Toyota Production System. They are:

  • Quantity Control – The ability of the system to adapt to daily and monthly fluctuations in demand in terms of quantity and variety.
  • Quality Assurance – Assurance that each process will supply only good units to subsequent processes.
  • Respect for Humanity – Cultivating Respect for Humanity while the system utilizes the human resources to attain its cost objectives.

Final Thoughts:

I will finish with an amusing article on Walmart. In this year’s shareholder meeting, Wal-Mart announced that they will stop playing Celine Dion and Justin Beiber in an effort to boost employee morale. Apparently, the stores were playing a CD with Celine Dion and Justin Beiber non-stop driving the employees crazy. This notorious playlist has been replaced with Wal-Mart Radio. This announcement received the most cheers from the crowd! This was based on multiple feedback from the employees.

Always keep on learning…

Innovation and Kaizen are not oil and water:

main

Kaizen is likely the most used Japanese word in the world of manufacturing. Kaizen simply means to improve for better. The “zen” part of Kaizen is not the same as the commonly known word “Zen”.

zen = virtue or good

Zen = literal meaning is “meditation”. This Japanese word has roots in the Sanskrit word “dhyan”.

It is quite possible to achieve Zen through kaizen. 🙂

This post is about the relationship between kaizen and innovation. Kaizen is often described as continuous improvement through small changes while innovation is described as a big change, or a complete breakthrough. The current paradigm is completely destroyed. From afar, these two concepts seem different – almost like oil and water.

What is the relationship between innovation and kaizen?

The book Kaizen Teian III (later published as The Improvement Engine) by the Japan Human Relations Association, states that kaizen cannot thrive without innovation.

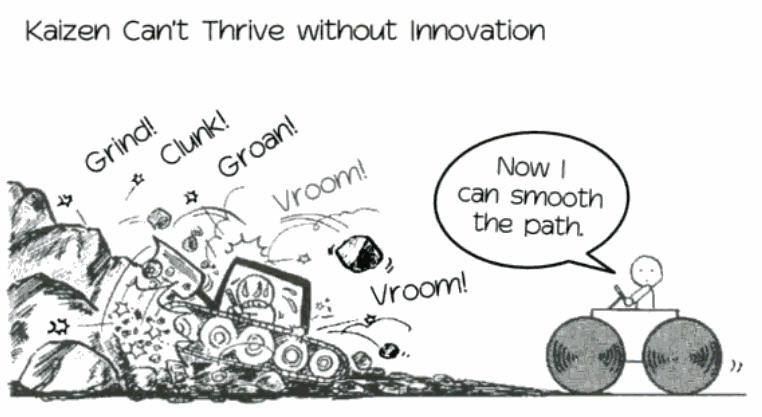
This is an interesting concept – if kaizen is continuous improvement through small changes, how can a company stay competitive just by making minor improvements? The book describes innovation as a bulldozer cutting a path through a rough terrain. Improvement activities are described as a means to leveling the path cut by the bulldozer, and paving it into a smooth road!

KIFigure taken from Kaizen Teian III.

The book further states that there is nothing more wasteful than trying to activate a kaizen system in a company that is not engaged in innovation! Trying to clear a path in a rough terrain with a pick and shovel will not do when you competitors are using a bulldozer.

My thoughts:

What is the purpose of kaizen?

There are two objectives for kaizen;

  • Continuous improvement to make work better
  • Development of employees so they can be better at problem solving and developing others.

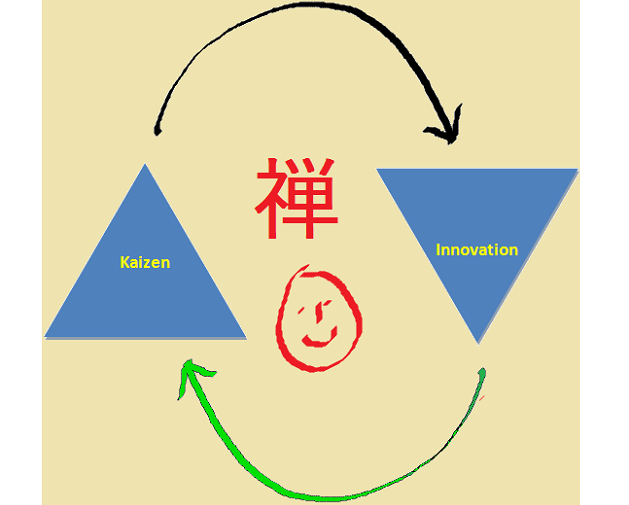
If kaizen can be described as a bottom-up process, then innovation can be described as a top-down process. You cannot move towards your ideal state (true north) without one or the other. You need both bottom-up and top-down forces to move towards your ideal state. They both create the perfect recipe for kaizen culture.

Always keep on learning…

In case you missed it, my previous post was about ESP and statistics.