A Brief Look at Kaizen in the Light of the Toyota Way:

chie to kaizen

I have talked many times in this blog about the “Toyota Way 2001”. The Toyota Way was an embodiment of Toyota’s management philosophy and values that were passed on to its employees as implicit knowledge. Due to rapid global expansion, Toyota Management decided to write down this implicit knowledge into a booklet – Toyota Way 2001, in order to help expand their production system properly across the globe.

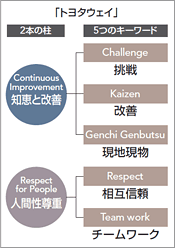
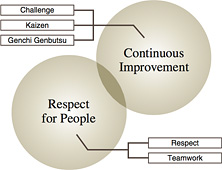
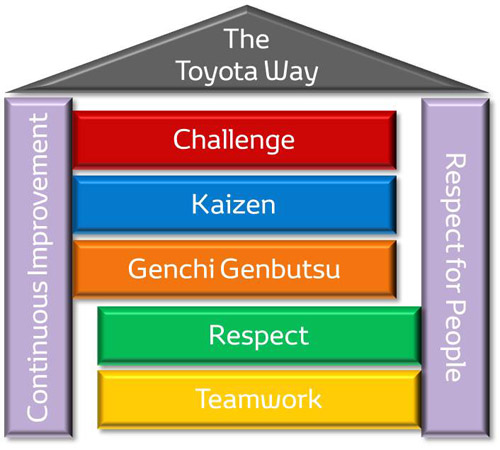
The Toyota Way has two pillars – “Continuous Improvement” and “Respect for People”. The “Continuous Improvement” pillar stands on three principles:

  • Challenge
  • Kaizen
  • Genchi Genbutsu

IMG_1282

All is good up to this point. “Kaizen” is often translated as “Continuous Improvement”. I saw this as a linguistic “chicken or egg situation”: How can kaizen be one of the three principles of “Continuous Improvement” when kaizen itself is “continuous improvement”? Why was the pillar not named simply as “Kaizen”?

Michel Baudin has written about it here. He has shown that the pillar is actually termed “Chie to Kaizen” in the Japanese version of Toyota Way 2001. “Chie to Kaizen” is translated as “Wisdom and Continuous Improvement”. I encourage the readers to check out Michel’s blog post.

Kaizen in Japanese is not translated literally as “continuous improvement”. The literal meaning is “change for better”. The Japanese word kaizen is derived from the Chinese word gaishan. They both mean “to improve”. Kaizen is written as 改善 in both Chinese and Japanese. This is because Japanese language uses a lot of characters adopted from Chinese language called Kanji. Apparently, to distinguish between “kaizen – improvement” and “kaizen – continuous improvement”, several Japanese writers have started using “カイゼン”, which reads the same. “カイゼン” is written in Katakana script, one of several writing components in the Japanese language, besides Kanji. Katakana is generally used for words imported from foreign languages. Thus when you translate the word “カイゼン” into English through Google Translator, you will find that the word translates to “Kaizen” in English. I am assuming that Kaizen in English means “Continuous Improvement.” 🙂
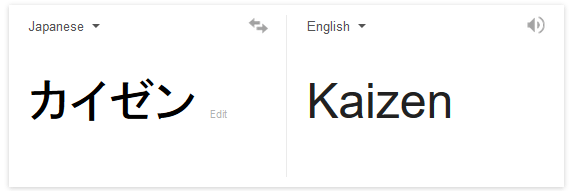
Kaizen

Wisdom/Intelligence and Continuous Improvement:

The only source where the pillar is not called as “Continuous Improvement” in English by a Toyota personnel that I could find, was “The Toyota Way in Sales and Marketing” by Yoshio Ishizaka. In this book, the first pillar is called as “Intelligence and Kaizen”. In my eyes, this is a better phrasing for the pillar. Ishizaka explains this pillar as follows;

Intelligence and Kaizen describes an attitude in which you are never satisfied with the current condition and continuously develop innovative ideas yielding higher added values.

Kaizen achieves a better meaning when viewed in the light of Challenge and Genchi Genbutsu. There is a sense of continuity towards improvement with this view. This meaning is more synonymous to “Continuous Improvement”. Let’s look at the other two principles: Challenge and Genchi Genbutsu.

Challenge: The key point here is to challenge the status quo. Do not be satisfied with your current state. There is almost always a better way of doing things. This may push you outside your comfort zones. But that is how you can continuously improve. This principle also encourages us to have a long term vision, and to move towards it at all times. As Toyota puts it “Working at Toyota is also an exercise in long-term thinking.”

Genchi Genbutsu: This is described as “going to the actual source and getting the actual facts” so that you can make the correct decisions. It is looked down upon in Toyota to make decisions based on data (on paper) alone. You have to be at the gemba to understand the problem.

My final words:

I will finish this post with a story I read that has the spirit of “chie to kaizen”.

Once upon a time a very strong woodcutter asked for a job from a timber merchant, and he got it. The pay was really good and so were the work conditions. The woodcutter was determined to do his best.
His boss gave him an axe and showed him the area where he was supposed to work. The first day, the woodcutter cut down 18 trees.

“Congratulations,” the boss said. “Go on that way!” Very motivated for the boss’ words, the woodcutter tried harder the next day, but he could only cut down 15 trees.

The third day he tried even harder, but he could only cut down 10 trees. Day after day he was bringing fewer and fewer trees.
“I must be losing my strength”, the woodcutter thought. He went to the boss and apologized, saying that he could not understand what was going on.

“When was the last time you sharpened your axe?” the boss asked.

“Sharpen? I had no time to sharpen my axe. I have been very busy trying to cut trees”, the woodcutter responded.

Always keep on learning…

In case you missed it, my last post was Don’t be an Expert at the Gemba.
Don’t Be an Expert at the Gemba:

Expert

In today’s post I will be talking about being open-minded at the gemba. I heard a wise saying;

“Minds, like parachutes, only work when open.”

parachute

I am sometimes guilty assuming that I know completely about the matter at hand – that I am an expert. I would be at the gemba and instead of listening to the operator talk, I would be talking to the operator, and trying to find solutions on my own. This type of thinking results in three things;

  • I am not respecting the operator or his expertise by not being open to his suggestions. The operator is truly the expert since he has been doing this, day in and day out.
  • By rushing to solutions, I am wasting the opportunity to develop the operator. By providing the solutions, I am taking away the privilege for the operator to think and come up with solutions.
  • I may not get his buy-in for what I am planning on implementing. Things will go back to the way they were once I leave that area.

Being an “expert” makes one close minded. It puts the blinders on for the person, and prevents them from seeing the whole. There is another side effect to being an “expert”. You become very comfortable at something and will not want to steer away from your comfort zone.

I have been reading books by Bruce Lee, the famed martial artist. Apart from being a great martial artist, Bruce was also a deep thinker. He talked about the great analogy of a cup that is applicable to this post:

“The usefulness of a cup is that it is empty.”

If a cup is not empty, it is not useful. The emptier the cup, the more useful it is!

Ohno and Experts:

Taiichi Ohno used to say that experts are not good for kaizen. “They would just get in the way”, he said. Ohno’s point about this statement is that experts would not be open to going outside their comfort zones, and they would not allow others to speak or be open to their ideas. Kaizen needs for you to be outside of your comfort zones. Comfort zones are the playgrounds for status-quos. This is against the spirit of kaizen.

In Toyota, there is a great concept called “chie”. Chie stands for “wisdom of experience”. If experience equates to expertise, then chie equates to wisdom that comes from experience. Toyota views their production system as a “Thinking Production System”. Toyota’s goal is to increase chie of all their workers so that their thinking leads to improved processes and this ultimately improves Toyota altogether. This type of thinking is against “experts” on the floor. Experience may result in improved efficiency, however this does not equate to improved effectiveness.

Final Words:

This post is more a reminder for me to be open minded at the gemba, and to listen to the operator, and to encourage them to ask questions and come up with solutions. This allows for developing the operator. This also allows you to learn from the operator as well. I will finish off with a short story from Leo Tolstoy about someone who thought he was an expert:

There once were three hermits on a remote island. They were known in the region for performing miracles. They were very simple, and did not know complicated prayers. The only prayer they knew was “We are three, Thou art Thee, have mercy on us.” 

One day the local bishop came to hear about the three hermits and their prayer. He thought to himself that he should pay them a visit so that he can teach them prayers that were “more correct”.

He arrived at the island and taught them the “state of the art” prayers. The three hermits recited the prayers after the bishop. The bishop was quite pleased with himself. He bid them good bye and left. His boat was sailing away from the island. It was getting dark. The bishop looked back at the island, and saw a radiant light slowly approaching the boat from the direction of the island. To his surprise, he saw that the three hermits were holding hands and running towards the boat, over the water.

“Bishop, we have forgotten the prayers you taught us”, they said, and asked him if he would please repeat them.

The bishop shook his head in awe at the miracle he was witnessing. “Dear ones”, he replied humbly, “Please forgive me, and continue to live with your old prayer!”

Always keep on learning…

In case you missed it, my last post was The Opposite of Kaizen.

The Opposite of Kaizen:

opposite_kaizen

“Kaizen” is the Japanese word that means “change for good”. Kaizen is probably the most used word in lean today. Kaizen has come to mean many things including “Kaizen events” – a week long group activity to improve a process. In today’s post, I am going to look at kaizen – the simple idea of “change for better” and look at what could be the opposite of kaizen. Kaizen is also translated as “continuous improvement”.

What is the Opposite of Kaizen? – Kaiaku

This is an interesting philosophical question. From a Japanese language standpoint, the opposite of kai-zen is kai-aku. In Japanese, Kai means “to change”, zen means “better” or “good” and aku means “bad” or “evil”. Thus kaizen literally means “change to be better” and kaiaku means “change to be worse”.

From a philosophical viewpoint, I do not agree that kaiaku is the opposite of kaizen. A person engaged in the kaizen mindset learns from failures as well. The fear of failure does not stop him from trial and error. Sometimes this activity can result in terrible failures – kaiaku. However, the mindset of kaizen is still alive. In fact, it is said that one learns the most from failures. Thus, kaiaku cannot be the opposite of kaizen. Failures which result in worse-of scenarios act as an impetus to make things even better.

What is the Opposite of Kaizen? – Kaikaku

Kaikaku translates from Japanese to English as “revolutionary change”. This is generally a large scale transformation. The intent behind kaikaku is that it is not a simple small scale change like kaizen. Toyota achieves improvement through both small scale and large scale improvements. They embrace both types. Toyota also embraces innovation (kakushin). From Toyota’s perspective any change that ultimately makes things better is always good! In this regard, the opposite of kaizen cannot be kaikaku either.

What would Ohno Say?

Taiichi Ohno, father of Toyota Production System, said the following about how to begin kaizen:

“You’ve got to assume that things are a mess.”

Ohno’s point behind this is that if you are happy and satisfied with where you are and what you are doing; you will never want to change. You have to be dissatisfied with what you are doing to motivate yourself in order to improve your process. The opposite of kaizen is complacency!

Being complacent means that you are happy where you are, and your goal is to maintain status-quo. In fact, Merriam Webster defines complacency as follows;

Complacency = self-satisfaction especially when accompanied by unawareness of actual dangers or deficiencies

This is the exact opposite of the intent behind kaizen – to improve/make things better. Complacency leads to stagnation, and ultimately this hinders survival. Dr. Deming is often misquoted with “It is not necessary to change. Survival is not mandatory.” His actual quote is;

“Learning is not compulsory; it’s voluntary. Improvement is not compulsory; it’s voluntary. But to survive, we must learn.”(Source: The Age of Stagnation, Satyajit Das)

There is an interesting anecdote in the Harvard Business Review article “What Working for a Japanese Company Taught Me”  by John E Rehfeld. John talked about his friend who was in charge of two factories, one in America and one in Japan. The Japanese factory always outperformed the American factory. His friend’s rationale was as follows:

“They both set the same target, and they both may hit it. But when the Japanese hit it, they keep going, whereas the Americans tend to stop and rest on their laurels before pursuing the next goal. So in the end, the Japanese achieve more.” They continuously strive for perfection with the goal of achieving excellence.

Final Words:

It is my view that although the opposite of kaizen from a linguistic standpoint is kaiaku, from a philosophical standpoint it is complacency. Complacency leads to stagnation, and makes one ignorant of the perils around. I talked about Leonardo da Vinci last time. I will finish off with a quote from him, and an anecdote involving Henry Kissinger and Winston Lord.

davinci

Iron rusts from disuse; stagnant water loses its purity and in cold weather becomes frozen; even so does inaction sap the vigor of the mind. (Source:The Notebooks of Leonardo da Vinci, Richte, 1888)

Winston Lord was working under the then National Security Advisor, Henry Kissinger. There were a lot of high priority national security projects going on at that time. Winston Lord was writing a special report for Henry Kissinger. He worked on it for days knowing how picky and critical Kissinger can be. Lord submitted the report to Kissinger. The report was immediately returned to Lord with a notation by Kissinger – “Is this the best you can do?”

Lord rewrote the report and polished it a little more. The report was again submitted, and almost immediately the report was sent back by Kissinger, again with the same question – “Is this the best you can do?”

Lord rewrote the report one more time and the report was again sent back with the same question. This time Lord snapped at Kissinger, “Damn it, yes, it’s the best I can do.”

“Fine. Then I guess I will read it this time”, Kissinger replied back.

Always keep on learning…

In case you missed it, my last post was Qualities of a Lean Leader.

Qualities of a Lean Leader:

leadership

In today’s post I will look at the qualities of a lean leader. I have been using the term “lean leader” in my posts. This is not an official title, and this does not mean “supervisor” or “manager”. A lean leader is someone who takes initiative in improving one’s process and in developing those around them.

I have wondered which qualities a lean leader needs. I believe that the best source for this is Michael J Gelb’s 1998 book, “How to Think Like Leonardo Da Vinci.”Michael researched Leonardo’s life and identified seven attributes to help one think like Leonardo Da Vinci. Michael listed them as Italian words to pay homage to the master. These are as follows;

  • Curiosità – An insatiable quest for knowledge and continuous improvement
  • Dimostrazione – Learning from experience
  • Sensazione – Sharpening the senses
  • Sfumato – Managing ambiguity and change
  • Arte/Scienza – Whole-brain thinking
  • Corporalità – Body-mind fitness
  • Connessione – Systems thinking

1) Curiosita:

curiosity-landed-drawing

Being curious is an essential attribute a lean leader should have. Being curious forces you to ask questions. Asking questions allows the other party to be involved. This leads to continuous improvement and discoveries. Michael defined this as “an insatiably curious approach to life and an unrelenting quest for continuous learning.”

2) Dimostrazione:

Soichiro Honda

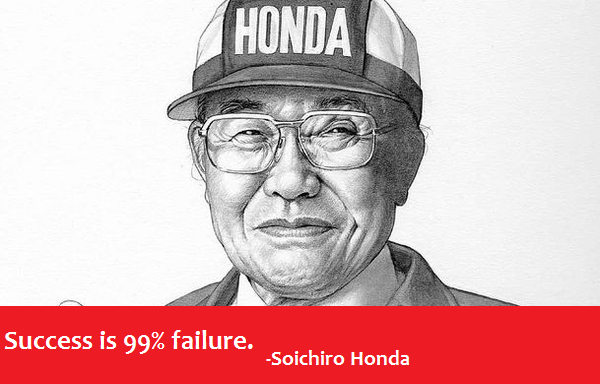
This can be described as a willingness to fail in  order to learn from mistakes. Michael described this as “a commitment to test knowledge through experience, persistence, and a willingness to learn from mistakes.”The example I have here is of Soichiro Honda. Soichiro did not have any formal education, and he went on to build Honda Motor Co.

3) Sensazione:

holmes

Taiichi Ohno would be proud of this attribute. Michael described this as “the continual refinement of the senses, especially sight, as the means to enliven experience.” As the lean learners know, Ohno was famous for his “Ohno circle”. Ohno used to teach supervisors, managers and engineers alike to learn to observe the wastes by making them stand inside a hand drawn chalk circle. They had to stay inside there until they start seeing the wastes like Ohno did.

4) Sfumato:

less is more
Sfumato refers to the style of painting Leonardo used. Sfumato is the technique of allowing tones and colors to shade gradually into one another, producing softened outlines or hazy forms. Michael described this as “a willingness to embrace ambiguity, paradox and uncertainty.” Toyota Production System has many paradoxes and counter-intuitive principles. Most of this is because of the trial and error methods that Ohno utilized. All of the manufacturing norms were challenged and broken.

5) Arte/Scienza:

IMG_1183

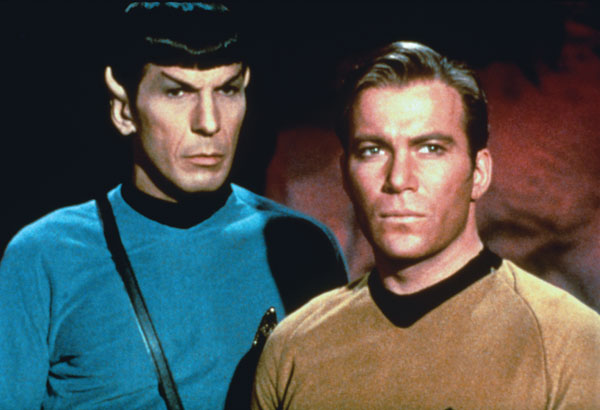
This attribute represents the synergy between art and science; logic and intuition. The classic TV show Star Trek played around this theme since the two main characters Spock and Kirk represented logic and intuition respectively. A lean leader needs both logic and intuition in order to develop oneself. Michael described this as “the development of balance between science and art, logic and imagination”.

6) Corporalità:

IMG_1186

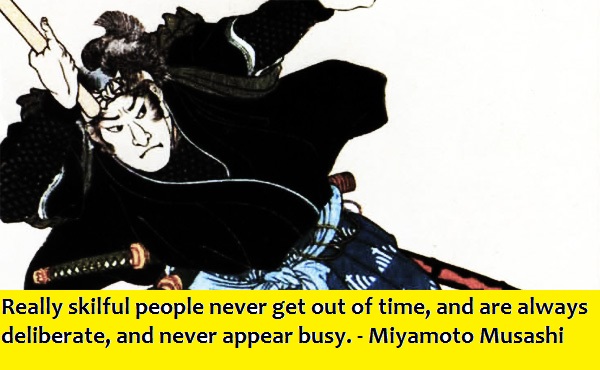
In the Book of Five Rings, Miyamoto Musashi talked about fluidity. “Really skilful people never get out of time, and are always deliberate, and never appear busy.”To me, this is the essence of Corporalita. Michael described this as “the cultivation of grace, ambidexterity, fitness and poise.” The quality of Corporalita is achieved only through constant practice as one strives towards their ideal state.

7) Connessione:

systems

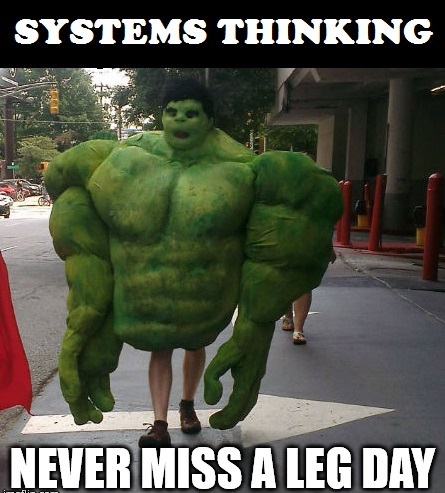
Dr. Deming and Eliyahu Glodratt would be proud to see this attribute on the list. This attribute is about “systems thinking”. Michael described this as “a recognition and appreciation for the interconnections of all things and phenomena.” A lean leader should be able to see everything from a big picture as well as a small picture view points. My favorite meme about Systems Thinking is the Never Miss A Leg Day meme. Local optimization of the just exercising the upper body leads to poor system optimization (muscular upper body and disproportionate skinny legs).

Leonardo, the Writer:

Leonardo da Vinci was also a writer. In his notebooks, he wrote numerous “jests” and fables. I will finish this post with a jest and a fable from the great mind of Leonardo Da Vinci:

A Jest:

It was asked of a painter why, since he made such beautiful figures, his children were so ugly; to which the painter replied that he made his pictures by day, and his children by night.

 The Tree & the Pole, A Fable:

 A tree which grew luxuriantly, lifting to heaven its plume of green leaves, objected to the presence of a straight, dry old pole beside it.

“Pole, you are too close to me. Can you not move further away?”

The pole pretended not to hear and made no reply.

Then the tree turned to the thorn hedge surrounding it.

“Hedge, can you not go somewhere else? You irritate me.”

The hedge pretended not to hear, and made no reply.

“Beautiful tree,” said a lizard, raising his wise little head to look up at the tree, “do you not see that the pole is holding you up straight? Do you not realize that the hedge is protecting you from bad company?

Always keep on learning…

In case you missed it, my last post was Dorothy’s Red Shoes and Toyota.

Dorothy’s Red Shoes and Toyota:

Silver red shoes

Today’s post is about the theme of adapting and not blindly copying something. Lean is the Western cultural interpretation of what is known as Toyota Production System (TPS). Many companies try to implement TPS by simply copying the tools without understanding the context behind them.

Dorothy’s red ruby shoes are cultural icons from the movie “The Wizard of Oz”. All Dorothy had to do to go home was click the heels three times and command to go home. Poof, like magic she returned home. It is not a widely known fact that Dorothy’s shoes in the actual L Frank Baum’s 1900 book were Silver. The shoes’ color got changed to look “iconic” using the new technology in those days – Technicolor. The shoes appeared extra magical when they were ruby red in the movie. In other words, the movie makers adapted the story to the new technology in order to bring out the best.

What did Toyota Do?

Toyota started off as a Loom Company. Kiichiro Toyoda, son of the founder of the Toyoda Automatic Loom Works, was interested in automobiles. Kiichiro started the Toyota Motor Corporation with little experience in large scale manufacturing. Toyota Production System has been tremendously studied and almost everybody tries to emulate Toyota. In those days, the best production system was Ford’s Mass Production System. It was very much akin to the lean manufacturing system today. In fact, Toyota sent Engineers to study the Ford Production System so that they could come back and implement it. One of the two Engineers sent was Eiji Toyoda, Kiichiro’s cousin, and later the Chairman of Toyota. Eiji was a strong supporter of Taiichi Ohno, the father of Toyota Production System.

Toyota was founded from the very beginning with aspirations to become the “Ford of Japan”.(Source: The Toyota Leader, Masaaki Sato 2008)

Toyota discovered that the Ford System as a whole did not work for them. The idea of a moving assembly line and the idea of an employee suggestion system were two concepts that Toyota adopted and started using. However, Toyota could not implement the “large scale” production practices that Ford was using. The Ford System was focusing on producing a limited product line in large quantities. It also focused on increasing the efficiency of each operation by making the lot sizes as large as possible. Inventory was considered as a buffer and a blessing to cover any production interruptions. Toyota simply did not have the capabilities to maintain a large scale production.

Taiichi Ohno found two main flaws in the Ford’s Mass Production System:

  • Only the final assembly line achieved anything resembling continuous production flow. At the component level, there were piles of inventory and very limited flow.
  • Ford was unable to accommodate customer preferences for product diversity. This is akin to the famous quote attributed to Ford – “You can have any color as long as it’s black.”

Source: The Japanese Automobile Industry, Michael Cusumano 1985.

Taiichi Ohno created the Toyota Production System by adapting ideas from Henry Ford, Sakichi Toyoda, Kiichiro Toyoda, and numerous others, including the inventor of the Supermarket System. He learned from failures and the production system evolved through numerous trials and errors. The Toyota Production System is a custom fit tailored suit that fits only Toyota, and nobody else. However, like Ohno did, we can certainly learn and adapt from it.

Why Should I Copy Toyota?

The short answer is – you should not blindly copy Toyota. You have to understand your problems, and then adapt the Toyota Production System and address the solutions to your problems. In an interview in 2001, Hajime Oba, a retired TPS Sensei said the following about blindly copying Toyota:

Big Three managers, he says, use lean techniques simply as a way to slash inventory and are satisfied with that. “What the Big Three are doing is creating a Buddha image and forgetting to inject soul in it,” he says.

My Final Words:

I will finish off with a lesson from the famous martial artist Bruce Lee and a funny story about the dangers of blindly copying. Bruce Lee is also considered to be a great philosopher as well.

His four steps for efficiency were;

  • Research your own experience
  • Absorb what is useful
  • Reject what is useless
  • Add what is essentially your own.

And now the story I heard as a kid in India;

A father was worried about his son’s lack of ability when it came to the English language. English was his son’s second language and he always had trouble with essay writing in the test. The father made his son memorize a short essay “My Best Friend”, since he was sure it would be part of the essay component of the test. The son learned the essay verbatim, and felt good about writing his essay for the test.

Unfortunately, the essay topic was “My Father”. The boy thought for a bit, and then started writing based on what he had memorized.

“I believe I have many fathers. Shankar Pramod is my best father. He lives a few blocks from my house. He comes to visit us every day. My mother loves him very much. A father in need is a father indeed.”

Always keep on learning…

In case you missed it, my last post was The Anatomy of an Isolated Incident.

The Anatomy of an Isolated Incident:

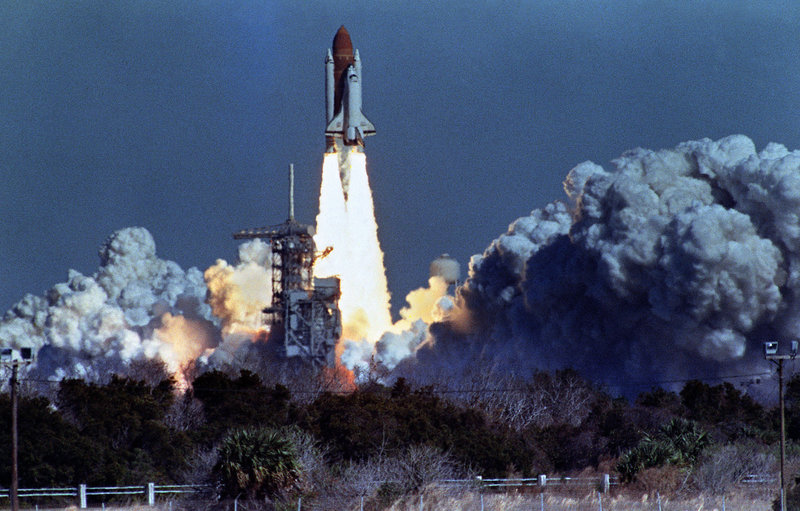
challenger

I read about the death of Bob Ebeling today. He was a NASA contract Engineer from Morton Thiokol who tried to stop the launch of the space shuttle Challenger in 1986. On January 26, 1986 soon after the launch, the Challenger was engulfed in flames. All seven crew members lost their lives in this terrible accident. Famous Nobel laureate Richard Feynman was part of Rogers Commission which investigated the Challenger accident.  Feynman wrote about this investigation in depth in his 1988 book “What Do You Care What Other People Think?”

In today’s post, I will be looking at Isolated Incidents. There are times in my career where I am taken aback by isolated events.  These events happen very rarely, and thus it is not easy to understand the root causes. I will use the Challenger accident as the primary example to look at this. There have been 135 NASA space shuttle missions between 1981 and 2011. Of the 135 missions, 133 flights went as planned, with two ending in disaster.

The O-Ring Fiasco:

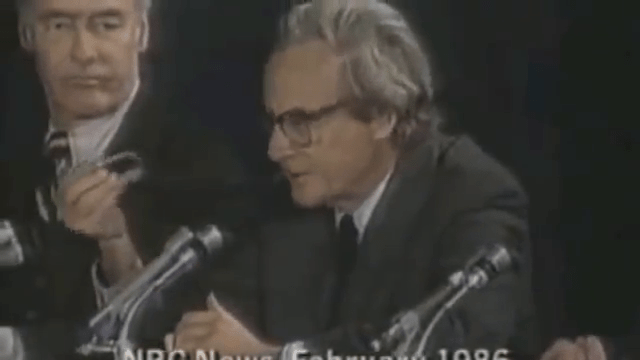
The Roger Commission identified that the Challenger accident was caused by a failure in the O-rings that were used to seal a joint on the right solid rocket booster. Bob Ebeling was among the group of Engineers who had warned NASA against the launch based on his concerns about the seals. The O-rings were not proven to work under cold conditions. It was noted that the temperature was below freezing on the day of the launch. Feynman famously demonstrated this by immersing an O-ring in a glass of ice water, and demonstrating that the O-rings were less resilient and that it retained its shape for a very short amount of time. This lack of resilience caused the failure of the seals leading to the Challenger catastrophe.

vlcsnap-2016-03-20-14h56m01s705

The Roger Commission indicated the following issues led to the Challenger accident:

  • Improper material used for the O-ring.
  • Lack of robust testing – the O-ring material was not determined to function as intended by NASA. Even though the O-ring manufacturer gave data to prove the lack of functionality at low temperatures, NASA management did not heed this.
  • Lack of understanding of risk from NASA management.
  • Potential push from management to launch the space shuttle to meet a rush deadline.

Feynman also wrote about the great disparity in the view of risk by the NASA management and the engineers. NASA management assigned a probability of 1 in 100,000 for a failure with loss of vehicle. However, when Feynman asked the engineers, he got values as low as 1 in 100. Feynman reviewed the NASA document that discussed the risk analysis of the space shuttle and was surprised to see extremely low probability values for failures. In his words;

The whole paper was quantifying everything. Just about every nut and bolt was in there. “The chance that a HPHTP pipe will burst is 10-7”. You can’t estimate things like that; a probability of 1 in 10,000,000 is almost impossible to estimate. It was clear that the numbers for each part of the engine were chosen so that when you put everything together you get 1 in 100,000.

Feynman also talked about an engineer being candid with him about his probability value of 1 in 300. He said that he calculated the risk as 1 in 300. However, he did not want to tell Feynman how he got his number!

The Anatomy of an Isolated Incident:

I have come to view the Isolated Incident cause-effect relationship as an equation. This is shown below.

Isolated Incident = Cause(s) + System weak points + Enabling Conditions

The Challenger Accident can be summarized:

Challenger Accident = Material limitation of the O-ring + NASA Management Policies + Cold conditions

The System Weak Point(s) are internal in nature. The enabling conditions, on the other hand, are external in nature. When you combine all the three factors in a perfect storm, you get an isolated incident. If we do not know all of the three factors, we are not able to solve the isolated incident. By itself alone, none of the factors above may cause the problem.

Another example is – when demand goes up, and production doubles. If the process is not robust enough to handle the spike in production, then isolated events can happen.

Pontiac’s Allergy to Vanilla Ice Cream:

I will finish this post with a fantastic story I read from Snopes:

The Pontiac division of General Motors received a complaint in the form of a letter. The letter was from a frustrated customer. He had been trying to contact the company for a while.

He wrote in the letter that he and his family were used to buying ice cream after dinner on a frequent basis. The type of ice cream that is purchased depended upon the mood of the family. He had recently purchased a new Pontiac car, and he had been having issues on his ice cream trips. He had figured out that the new car is allergic to vanilla ice cream.

If he purchased any other flavor, his car would start with no problem. However, if he purchased vanilla ice cream, his car will not start.

“What is there about a Pontiac that makes it not start when I get vanilla ice cream, and easy to start whenever I get any other kind?”, he asked in the letter.

The letter was delivered to the Pontiac President who was very amused by it. He sent an engineer to investigate the fantastic problem. The engineer went with the family three nights to get ice cream in the new car. The first night the family got chocolate ice cream, and the car started with no problem. The second night, they got strawberry. The car again was fine. On the third day, the family got vanilla ice cream; lo and behold the car would not start.

This was repeated on multiple days, and the results were always the same. The engineer was a logical man, and this stumped him. He took notes of everything. The only thing that he could see was time. The family always took the shortest amount of time when they purchased vanilla ice cream. This was because of the store layout. The vanilla ice cream was quite popular and was kept at the front of the store. Suddenly, the engineer identified why the isolated incident happened. “Vapor lock”, he exclaimed. For all the other flavors, the longer time allowed the engine to cool down sufficiently to start without any issues. When the vanilla ice cream was bought, the engine was still too hot for the vapor lock to dissipate.

Always keep on learning…

In case you missed it, my last post was Kintsukuroi and Kaizen.

Kintsukuroi and Kaizen:

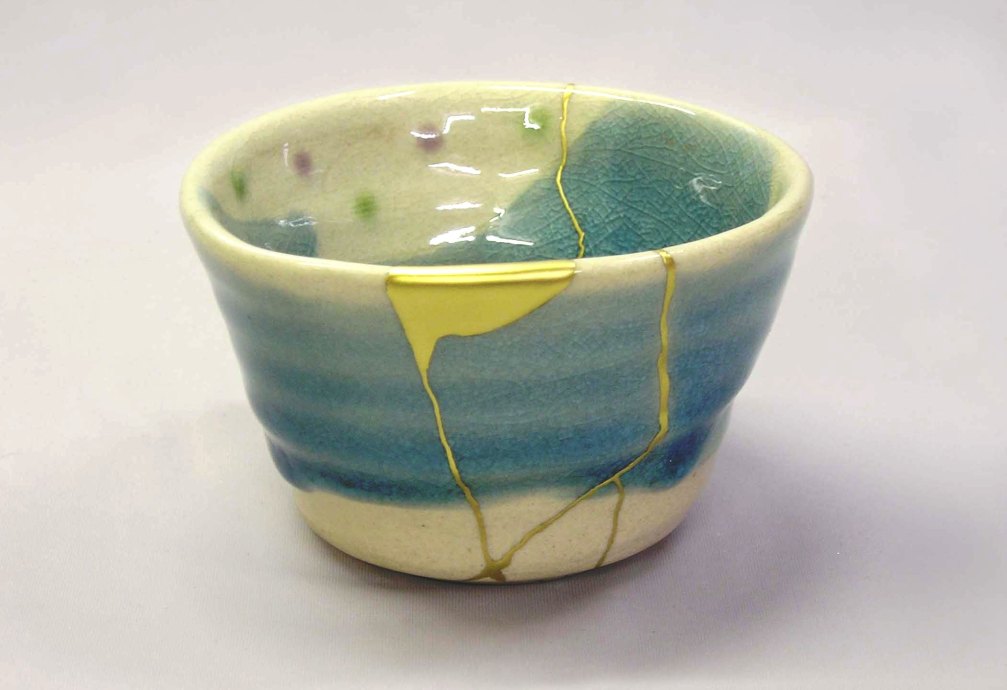
kintsukuroi_tunasima

In today’s post, I will look at kintsukuroi and how it applies to lean. Kintsukuroi can be translated from Japanese as “to repair with gold”. This process converts broken ceramic pieces to beautiful art forms. The damaged piece is not thrown away, but is embellished by filling the cracks with a lacquer mixed with gold dust. The final product becomes more valuable than the original.

The Origin Story of Kintsukuroi:

There are several versions of the origin story.

Toyotomi Hideyoshi was a ferocious military ruler in Japan during the 1500’s. He was well known for his quick temper.

He hosted tea ceremonies which were well attended. He was particularly fond of a Korean Ido-style tea bowl. One day, a page handling the bowl accidentally dropped it and it broke into several pieces. Hideyoshi was furious at the page, and everybody feared for the poor page’s life.

One of the guests calmed the military ruler, and went away with the broken pieces of the bowl. He returned after a few days with a fully restored bowl that was “repaired with gold”. Hideyoshi was blown away by the beauty of the restored bowl, and he loved the repaired bowl even more. The repaired bowl was more valuable, more beautiful and became more cherished.

What can we learn from this?

I have been learning about Japanese culture for some time now and the concept of kintsukuroi fascinates me. The readers of my blog know that I enjoy connecting things together. I believe that the concept of kintsukuroi creates a new perspective on Kaizen.

As a lean leader, we should look at breaking the current process, and restoring it through process improvements (Kaizen). We are sometimes too close to the action that we fail to see the wastes in the process. We believe that the current process is adequate as is. We may not see opportunities to improve.

However, we should break apart the bowl, and restore it with gold. We should evaluate the process through the steps of ECRS:

  • Are there any steps we can Eliminate?
  • Are there any steps that we can Combine?
  • Are there any steps that we can Rearrange?
  • Are there any steps we can Simplify?

This is the basic idea of Kaizen. The new process should be more valuable than the old process, in that it has fewer wastes and it utilizes the available resources efficiently and effectively.

Each kintsukuroi process is unique. Similarly each process improvement activity is unique. One should understand the problem first and apply solutions. To understand the problem, one must break apart the process (bowl). Once the process is broken apart, one should utilize Kaizen thinking (gold lacquer mix) and put the process back together.

Always keep on learning…

If you enjoyed this post, you can read more here.

In case you missed it, my last post was What is my purpose?

What is my purpose?

purpose

Peter Drucker declared in his 1954 book “The Practice of Management” that the purpose of a business is to create a customer. In today’s post I will talk about purpose, specifically what do I think my purpose is at work? There is of course the utilitarian answer about my purpose at work – to fulfill my job duties/responsibilities. However, fulfilling the job duties/responsibilities does not always complete my purpose.

The purpose is to create/increase value in anything I do:

Peter Drucker in the book “The Practice of Management” talks about understanding customers. He notes that the manufacturer of gas kitchen stoves should not consider himself to be in competition with only other gas kitchen stove manufacturers. The customer is not just buying a stove. The customer is looking for the easiest way to cook food. There are many forms of stoves/utensils available to the customer that are in direct competition. There are several different ways to cook food including microwave ovens, cooking ranges, grills, etc. Ignoring them will result in loss of business. This example may be outdated. However, the core idea is applicable here. If you are simply fulfilling just your basic job duties/responsibilities, you are like the gas stove manufacturer. You will not grow and develop yourself if you just stick to your defined duties/responsibilities and you will eventually get passed by.

Your purpose is to create/increase value in anything you do. From a Toyotayesque philosophy, this is similar to the Continuous Improvement attitude. You are always trying to improve what you are doing. You are expanding your boundaries and you have a responsibility to develop yourself. One of the two pillars for the Toyota Philosophy identified in the Toyota Way 2001 is “Continuous Improvement”. The first key concept for “Continuous Improvement” is the “Spirit of Challenge”. In Jeffrey Liker’s “The Toyota Way to Lean Leadership”, Liker talks about the Spirit of Challenge as follows;

“Like the two founding Toyoda family members, every Toyota leader is expected not just to excel in his current role but to take on the challenges to achieve a bold vision with energy and enthusiasm.”

toyotaway_img01

The two Toyoda family members are Sakichi Toyoda and Kiichiro Toyoda. I have referenced them in my last two posts. It is likely that Liker meant every Toyota employee when he said Toyota leader. This type of thinking is instilled from an organization standpoint. To quote Peter Drucker again;

“Most people need to feel that they are here for a purpose, and unless an organization can connect to this need to leave something behind that makes this a better world, or at least a different one, it won’t be successful over time.”

Toyota has a core concept of True North. True North is your ideal state. You can never truly achieve this. However, it is your responsibility to strive moving towards your True North.

Final Words and a story on purpose:

I am a firm believer of taking responsibility and authority to do the right thing, and to develop yourself. One must always try to increase/add value in what they do. Increasing value in what you do ultimately increases your value. This is the Spirit of Challenge. This is your inner purpose.

I will finish off with an anecdote, I heard from the Indian author Shiv Khera (in his words).

16 years ago in Singapore I gave a taxi driver a business card to take me to a particular address. At the last point he circled round the building. His meter read 11$ but he took only 10.

I said Henry, your meter reads 11$ how come you are taking only 10.

He said Sir, I am a taxi driver, I am supposed to be bringing you straight to the destination. Since I did not know the last spot, I had to circle around the building. Had I brought you straight here, the meter would have read 10$. Why should you be paying for my ignorance?

He said Sir, legally, I can claim 11$ but ethically I am entitled to only 10. He further added that Singapore is a tourist destination and many people come here for three or four days. After clearing the immigrations and customs, the first experience is always with the taxi driver and if that is not good, the balance three to four days are not pleasant either. He said Sir I am not a taxi driver, I am the Ambassador of Singapore without a diplomatic passport.

In my opinion he probably did not go to school beyond the 8th grade, but to me he was a professional. To me his behavior reflected pride in performance and character. That day I learnt that one needs more than professional qualification to be a professional.

Always keep on learning…

In case you missed it, my last post was Toyota Production System House – Just-in-Time (JIT) and Jidoka (Part 2).

Toyota Production System House – Just-in-Time (JIT) and Jidoka (Part 2):

jidoka

I talked about the two conceptual houses of Toyota last week. In today’s post we will look JIT and Jidoka, the two pillars of the Toyota Production System house. The two pillars of the TPS house are actually based on the ideas of Sakichi Toyoda (Jidoka) and Kiichiro Toyoda (JIT). Ohno built his production system on the shoulders of these two giants.

Sakichi Toyoda, father of Kiichiro Toyoda, founded Toyoda Automatic Loom Works in 1926. Sakichi was an inventor and considered to be an eccentric (Source: Fifty Years in Motion, Eiji Toyoda 1985). His greatest invention was perhaps the Type G Automatic Loom, a non-stop shuttle change automatic loom. Sakichi sold the license to the Platt Brothers and Co. in England.

There is a great story about Sakichi Toyoda in Eiji Toyoda’s book, regarding the automatic loom invention. The looms used to be manually operated and were made of wood. Sakichi wanted to create a loom that ran on power. The best power source in his days was steam. He purchased a used steam engine to understand how it worked and to use that to power his looms. The looms however did not move because the steam kept leaking. Sakichi took the engine apart and found that the problem was worn down piston rods that caused the steam to leak. This would be an easy fix to have new rods turned down on a lathe. Sakichi, however, did not have access to a lathe. So Sakichi and his team spent a whole night manually filing the rods down! When they put the rods in the engine, it worked.

Kiichiro Toyoda, Sakichi’s son, formed an automotive division under Toyoda Automatic Loom Works. He later spun this off, and created Toyota Motor Company in 1937. He calculated that with a population of one hundred million people in Japan, a car-to-people ratio of 1:10 would equate to ten million cars. If there was a 10 percent replacement per year, this would equate to one million cars. He thought that this was a good reason to start a car company.

Just-in-Time:

Kiichiro Toyoda, who founded the Toyota Motor Corporation, had come up with the idea of making the right parts at the right time, and in the right amount. In those days, the norm was to use a lot production system. This is based on producing parts according to what the operation can produce. Thus, there was a disjoint between what is actually needed, and what the operation produced. The operation tended to produce as much as it could to be efficient. This led to high inventories, which led to large stock rooms to store these inventories. Kiichiro understood that this automatically increased the cost to run the business, something that Toyota struggled with tremendously in the beginning. He decided to switch over entirely to a flow-type production system. He called this the “just-in-time” concept:

“I believe that the most important thing is to ensure that there is neither shortage nor excess, that is, to ensure that there is no excess labor and time for the designated production. There is no waste and there is no excess. It means not having to wait for parts to be circulated around. For Just-in-Time, it is important that each part be ready ‘just in time’. This is the first principle of increasing efficiency.” (Source: July 1938 issue of Motor, Toyota-Global website)

“Just make what is needed in time, but don’t make too much.” (Source: Fifty Years in Motion, Eiji Toyoda 1985)

Kiichiro wrote a four inch binder manual detailing his ideas for JIT. His ideas were used at Toyoda Automatic Loom Works, which is where Taiichi Ohno first joined Toyota at. Kiichiro tried to implement this at the Koroma plant, Toyota’s second automotive manufacturing facility. It did not take hold at the Koromo plant due to part shortages when the war with China (2nd Sino-Japanese War and World War II) expanded into the Pacific. It is said that Eiji Toyoda, Kiichiro Toyoda’s cousin, requested Ohno’s help to implement Just-in-Time at the Koroma plant.

“Mr. Ohno”, Eiji said, “this plant looks like a storeroom. Can you do something to take care of this?” Eiji wanted to pleasantly surprise the big man (Kiichiro Toyoda) and show that Just-in-Time was already in operation at the Koroma plant. (Source: The Toyota Leaders, Massaki Sato.)

It should be noted that Eiji Toyoda was a strong supporter of Taiichi Ohno, and stood behind him when he was developing the system. In Taiichi Ohno’s words – “Our approach has been to investigate one by one the causes of various unnecessaries in manufacturing operations and to devise methods for their solution, often by trial and error.”

Ohno would later on create the Kanban system to incorporate the Just-in-Time philosophy.

Jidoka:

Jidoka in Japanese stands for “automation”. Toyota added an extra character representing “human” in Japanese to mean “autonomation” or “automation with a human mind”. In Japanese, both words can be expressed as “Jidoka”. The word autonomation comes from joining “autonomous” and “automation”.

There are two approaches to autonomation at Toyota. The first approach is to separate the operator’s work from the machine’s work. This means to treat the operator as being independent of the machine, or in other words the operator can operate multiple machines simultaneously. The norm had been to have one operator dedicated to one machine only. The operator had to watch the machine work, while not creating value at the same time. In his mind, he was creating value by simply watching the machine operate. The second approach is to have the machine detect an anomaly and stop by itself. This would prevent the machine from producing more defects. Additionally this will also force the operator to fix the problem immediately to maintain the flow of the process. Both of these ideas belonged to Sakichi Toyoda, father of Kiichiro Toyoda. His Type G loom was an automatic loom that stopped on its own when any of the threads broke. Thus, the loom did not continue producing defectively. Sakichi had successfully implemented the two approaches at the Toyoda Automatic Loom Works. At the Toyoda Automatic Loom Works, one operator could operate 25 automatic looms at the same time.

Soon after World War II, Kiichiro declared the company goal of catching up with America’s productivity within 3 years. In order to do this, Taiichi Ohno used the idea of having an operator in charge of multiple machines at a time. This increased the productivity by many fold. However, this came with its own problems. The machines were not aligned properly so that when the machine was done with its operation, instead of stopping it kept on making parts. Additionally, if the machine malfunctioned, it continued making defective parts. Thus, even though the productivity increased, it put a strain on process flow and quality.

In order to counter the flow problems, Ohno utilized machine layout and limit switches so that the machine stopped producing when the required amount of parts were produced. For the quality problems, Taiichi Ohno utilized the second approach of Jidoka, to have the machine stop production on its own when there is a problem or when the required quantity is made. This idea of Jidoka is to build in quality, ensuring that defective parts are not passed to the next station. This theme evolved into empowering the operator and giving him the authority and responsibility to stop the line if they identified a problem on the line. The operator would pull on the andon cord which would trigger an audio and visual signal for the lead or supervisor to come and help in fixing the problem. If the problem is not fixed in the allotted time, the entire line will stop until it is fixed.  Jidoka develops the operators to look for problems and then solve it. Jidoka thus evolved into a strong training tool and an employee empowerment tool for Toyota. Jidoka placed a spotlight on problems.

Final Words:

Ohno created the Toyota Production System based on the ideas from Kiichiro Toyoda (Just-in-Time) and Sakichi Toyoda (Stop on Defect).  It should be noted that all of the “tools” in TPS were created for the two pillars to work effectively. At first, the goal of TPS was to increase productivity to catch up with Detroit. However, as the productivity increased, it became necessary to maintain quality, and to ensure that the employees are challenged to continuously improve their processes.

I will finish off with an Ohno story. This was told by Michikazu Tanaka in the 2009 book “The Birth of Lean.”

Ohno was very interested in the Supermarket system that was in America. Ohno explained with passion to Tanaka how Toyota can utilize the concept of a Supermarket. Tanaka could not quite grasp the concept since supermarkets were still a foreign concept in Japan, where the shopkeepers fetched the items for the customers. Tanaka was amazed that the shopkeepers would let the customers freely pick what they want from the display, and pay as you go out.

“What would happen,” he asked Ohno, “if someone went in and ate a bunch of food without paying?”

Ohno was stumped and he did not have a good answer for Tanaka. He thought for a while, and said “I suppose that Americans are a people of integrity and they would know not to do that!”

Later on when Ohno implemented kanbans, he told the people on the floor “Kanban is like money; if you take out parts without kanban, you are stealing the parts”. (Source: The Evolution of a Manufacturing System at Toyota, Fujimoto)

Always keep on learning…

In case you missed it, my last post was The Two Houses of Toyota.

The Two Houses of Toyota (part 1):

2

Toyota is famous for manufacturing automobiles. You may not know that Toyota also builds residential houses. You can learn more about it here. I will not be talking about the real livable Toyota houses today. I will be talking about the “conceptual” Toyota houses.

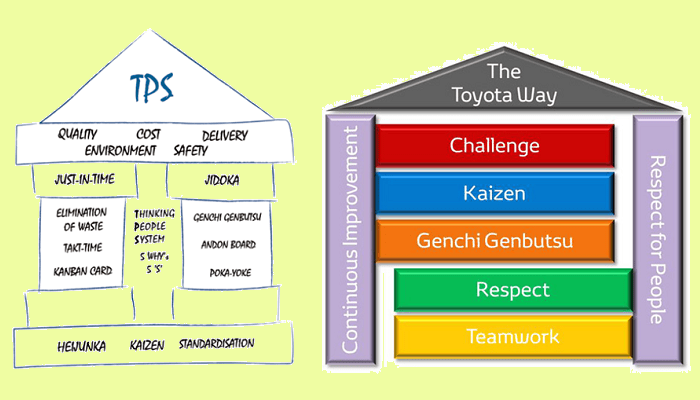
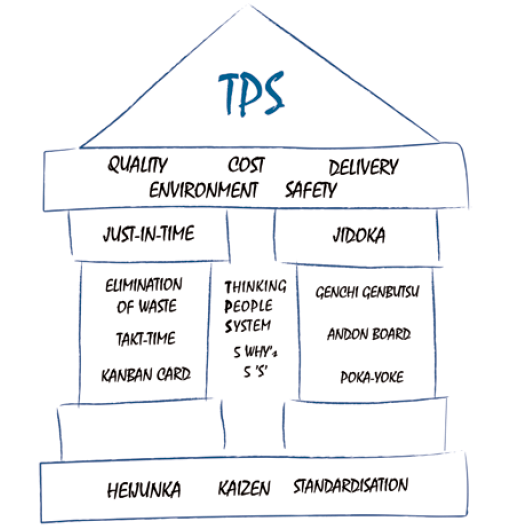
A lean enthusiast is familiar with the Toyota Production House. The house has two pillars – Jidoka and Just-in-Time. In 2001, Toyota revealed their organization’s guiding principles known as the Toyota Way. The Toyota Way also has two pillars – Continuous Improvement and Respect for People. There are literally thousands of depictions of the Toyota houses available online. The majority of these were created by non-Toyota people. I wanted to use only the depictions from a Toyota website.

The first house is the “Toyota Production House”. The picture below is taken from a Toyota Europe Forklift brochure. The reader can click on the picture to open the link to the brochure.

TPS

The second house is the “Toyota Way” house. The house below is taken from the Toyota Italy website. The reader can click on the picture to open the link.

way

First Descriptions of the Pillars:

From what I could find, the two pillars of TPS were first described officially in the “The first book of Toyota Production System”, an internal document released in 1973. The two pillars were later described in Taiichi Ohno’s 1978 book – “Toyota Production System”. Detailed descriptions of Respect for People and Continuous Improvement can also be found in the “The first book of Toyota Production System.” However, the Toyota Way house was not described in these earlier documents as it is currently.

It is interesting to note that starting in 1945, Taiichi Ohno began developing the Toyota Production System, but did not have the system documented until later. Norman Bodek, in his Foreword to Taiichi Ohno’s book “Toyota Production System” speculated that Ohno had feared Americans would discover his ideas and use them against the Japanese.

Fujio Cho, who was one of the people behind “The first book of Toyota Production System”, co-authored the 1977 paper “Toyota production system and Kanban system, Materialization of just-in-time and respect-for-human system”. This paper is available here. The roots of Toyota Way can be found in the paper. The section below is taken from the paper, and it is evident that Fujio Cho, the main architect of the Toyota Way 2001, had been thinking about the strategy for Toyota Production System:

Toyota is planning and running its production system on the following two basic concepts. First of all, the thing that corresponds to the first recognition of putting forth all efforts to attain low cost production is “reduction of cost through elimination of waste”. This involves making up a system that will thoroughly eliminate waste by assuming that anything other than the minimum amount of equipment, materials, parts, and workers (working time) which are absolutely essential to production are merely surplus that only raises the cost. The thing that corresponds to the second recognition of Japanese diligence, high degree of ability, and favoured labour environment is ” to make full use of the workers’ capabilities”. In short, treat the workers as human beings and with consideration. Build up a system that will allow the workers to display their full capabilities by themselves.

The Relationship Between the Two Houses:

Simon Dorrat, Manager of Toyota’s Business Intelligence function (2008 – 2013), has succinctly summed up the relationship between the two houses:

“The Toyota Production System is a practical expression of The Toyota Way – principles that guide everything we do in Toyota, based on Continuous Improvement and Respect for People.”

The Toyota Way 2001 represents the “What” and the “Why”, while the TPS House represents the “How”. In some ways this is akin to strategy and tactics.

Final Words – Even Ohno is fallible:

I will be exploring the pillars of the two Toyota houses in the future. I will finish this post with an Ohno story about Jidoka, one of the two pillars of the TPS house.

Even though Taiichi Ohno was a proponent of Genchi Genbutsu (Going to Gemba to learn actual facts), he was not infallible at this. Taiichi Ohno opened up in an interview with Michael Cusumano, author of the 1985 book – “The Japanese Automobile Industry – Technology and Management at Nissan and Toyota”. Ohno revealed that he had never tried to operate more than one machine at a time to see if it is easy or hard.

As part of implementing Jidoka at the Toyota automobile facility (Koroma plant), Ohno separated the operator’s work from the machine’s work. He treated the operator as being independent of the machine, and he had the operator work multiple machines simultaneously. The norm had been to have one operator dedicated to one machine only. The operator felt that he was creating value by simply watching the machine operate. Ohno understood that the operator is not adding value by watching over the machine. However, the operators hated operating several machines at once. Ohno admitted to Michael that he never felt the need to try operating several machines simultaneously to see how easy or hard it was. (Source: The Japanese Automobile Industry – Technology and Management at Nissan and Toyota, Michael Cusumano). Perhaps, it was because Ohno knew that the technique of one operator managing multiple machines was already successfully implemented at Toyoda Automatic Loom Works by Sakichi Toyoda, father of the founder of Toyota Motor Corporation. Ohno started at Toyota by working for the Loom Plant.

Ohno would later add in the interview that “Had I faced the Japan National Railways union or an American Union, I might have been murdered.” Ohno did have the support of the employee union at Toyota, as well as the upper management. Thus there was no immediate danger to Ohno’s life.

Always keep on learning…

In case you missed it, my last post was Wizard of Oz, Camel’s Nose and Being a Change Agent.