Dharma, Karma and Quality:

Dharma

In today’s post I will be looking at the statement – quality is everyone’s responsibility. This is an interesting preachy statement. There are two questions that can be answered by this statement;

  1. Who is responsible for quality?
  2. What is everyone responsible for?

The first question (who is) is a wrong question to ask because it leads to blaming and never results in an improvement of current state. The second question is just too broad to answer. Everyone is surely responsible for more than just quality.

Dharma and Karma:

The best way to explain responsibility is by looking at “dharma”. “Dharma” is an ancient Sanskrit term, and goes back to about 1500 BC. The word was first explained in the ancient Indian script Rig Veda. This was explained as a means to achieve a sense of order in the world. The term loosely can be translated as “responsibility”, or “something that needs to be done from a sense of duty”. The main purpose of dharma is to preserve or uphold the order in a system. For example, the dharma of a plant is to bloom.

This brings me to the next word – “karma”. “Karma” is more commonly used in the English language, and everybody has some understanding of this word. The term actually means “action” in Sanskrit. The action can be in the past, present or in the future. However, every one of your actions has a consequence. This attaches the “cause and effect” meaning to the word “karma”.  There are three types of karma identified in the Sanskrit texts;

  1. Karma = action
  2. Vikarma = wrong action
  3. Akarma = no action (doing nothing is a form of action, and sometimes this is the right thing to do)

If everybody performs karma according to their dharma, then the system is sustained successfully.

Top Management – 85% or 100% Responsible?

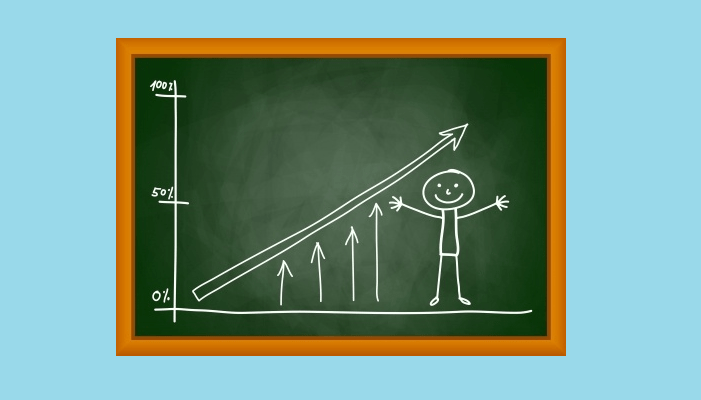
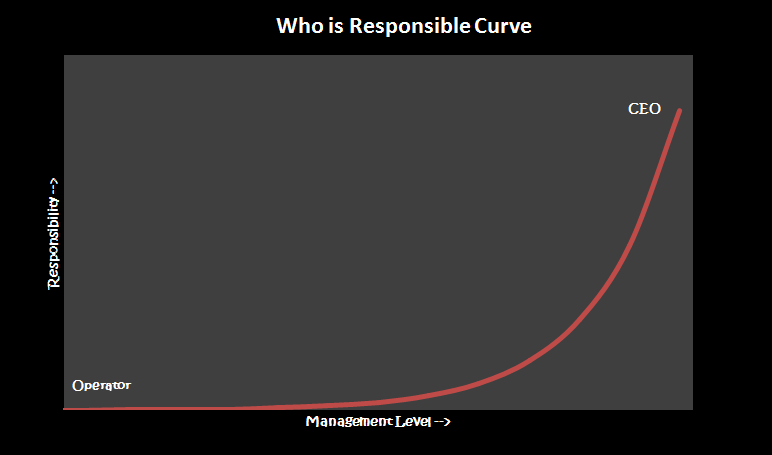
The answer to the question, “who is responsible for quality” is sometimes answered as “Top Management”. Dr. Deming taught that “85% of all quality problems are management problems”. He is also supposed to have stated “85% of TQC’s (Total Quality Control program) success depends on the president.” This can be depicted as the chart below.
Responsibility

I have viewed this as – patient zero is in the board room.

Taiichi Ohno’s, the father of Toyota Production System, view on this was as follows;

“In reality, TQC’s success depends on the president’s resolution to assume 100% responsibility. The president should imagine him or herself taken hostage by TQC and become devoted to human quality control.”

Dr. Deming has also said that – Quality is made in the board room. However, he goes on to clarify this. Quality is everyone’s responsibility, but top management has the most leverage of all to make a meaningful impact with their decisions.

In this light, the answer to the question – “what is your responsibility?” is “You are responsible for what you can control.”

Top management’s dharma is to lay down the framework for the entire organization to grow. This involves strong vision, big and drastic improvements (innovation) and growth. Middle Management’s dharma is to enforce and reinforce the framework through maintaining the status quo while encouraging small improvements (kaizen) and developing people. The operator’s dharma is to aid middle management to maintain status quo while looking for opportunities for improvements. The push for maintaining status quo is to provide a temporary structure for the process so that it can be studied for improvements. The main goal is destruction of the status quo so that a new standard can be achieved. If the karma aligns with the dharma, then the organization will sustain itself, grow and be successful.

Final Words:

I have recently rediscovered Dr. Deming’s definition of quality – Quality is the pride of workmanship. I will use Dr. Deming to succinctly summarize this post.

“In a well organized system all the components work together to support each other. In a system that is well led and managed, everybody wins. This is what I taught Japanese top management and engineers beginning in 1950.”

I will finish off with a Zen monk story;

A monk was driving his car when a dog from nowhere crossed the road. Although the monk tried stopping his car, he ran over the dog, killing it. The monk stopped his car and parked it. He looked around and saw a temple across from the road. He went to the temple and knocked at the door. Another monk opened the door.

The first monk bowed his head and said “I am so sorry.”

He pointed to where the accident happened and continued; “My karma ran over your dogma over dharma”. (My car ran over your dog over there.)

Always keep on learning…

In case you missed it, my last post was To Be or Not To Be.
To Be or Not To Be:

decide

In today’s post, I will be looking at the process of decision making and the use of a modified Pugh Chart to quantitatively conduct decision making.

The general process for decision making looks like something below;

  1. What do I have to decide? What is it about?
  2. What are my choices?
  3. What are the pros and cons for each?
  4. Act upon the decision and see if any further action is needed.

Decision Making is an Emotional Process:

As you go deeper into the decision making process, you can see that it gets more and more interesting. The neuroscientist, Antonio Damasio made the striking discovery that decision making is emotional in nature, and is rarely logical. He studied several patients who suffered injuries to their brains which impaired their emotions. Their reasoning capabilities were not impacted. They all had difficulty making decisions. The patients were all cognitively normal except that they had lost their ability to experience emotions, and this significantly impacted their ability to make decisions.

So at the point of decision, emotions are very important for choosing. In fact even with what we believe are logical decisions, the very point of choice is arguably always based on emotion.   

Complexity in Decision Making:

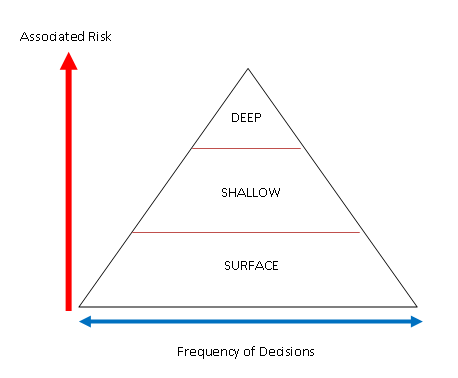
As a leader in your organization, you are required to make decisions on a daily basis. The types of decisions can be broken down into three classes;

  1. Surface – Simple situations requiring routine decisions
  2. Shallow – Complicated situations requiring supervisorial or managerial level decisions
  3. Deep – Complex situations requiring Upper management level decision making

This approach is adopted from Bennet and Bennet. The surface decisions are made on a daily basis, and do not have a high risk associated with them. The shallow decisions are more infrequent and have a medium level of risk associated with them. Finally, deep decisions are rare and have high risk associated with them.

bennet

Jeff Bezos, founder of Amazon.com, talks about a similar approach. He argues that there is no one-size-fits-all approach for decision making. In his opinion, there are two levels of decisions to be made. “Type 1 decisions” are those decisions that have critical consequences and are irreversible or nearly irreversible. He calls them “one-way doors”. He advises making Type 1 decisions carefully, slowly and with great thought and deliberation. The other kind is the “Type 2 decisions”. These are simple and easily reversible decisions. These decisions should be made much faster and frequently. A wise man knows the difference between the two.

To Include or to Exclude:

When you think about it, decision making is a process of deciding whether to include or exclude something. I came across a great article on this involving the custom of arranged marriages in India. The decision making process in an arranged marriage uses the approach of inclusion or exclusion. The two types of thinking are;

  • Inclusion – After careful thought, out of the 100 applicants choose the few that you think are most suitable for your child.
  • Exclusion – After careful thought, out of the 100 applicants eliminate the applicants that you think are not suitable for your child.

The counterintuitive outcome is that if you utilize the inclusion approach, you will select much fewer candidates. If you use the exclusion approach, you will retain a higher number of candidates, even though you are using eliminating criteria. Additionally, when the exclusion approach is used, you are highly likely to choose an “average” candidate. On the other hand, when the inclusion approach is used, you are highly likely to choose a candidate who is very strong in certain categories.

Quantitative Pugh Matrix Method:

My favorite tool for decision making is a version of the Pugh Matrix method. The steps for the Pugh Matrix are as follows;

  1. Decide upon the categories that are most important for making the decision
  2. Assign a weighted scale for each category
  3. Choose a scale for each category. This can be 1 – 5, where 1 = worst and 5 = best
  4. Score each category for the different options
  5. Find the final weighted score for each option. The option with the highest weighted score wins.

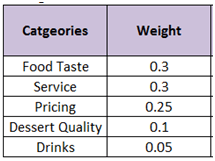
As an example, let’s look at the highly complicated decision of where to go for dinner. The following categories maybe suitable for this example – food taste, service, pricing, dessert quality and drinks. The next step is to assign the weighted scale. The sum of all the weighted scales should add up to 1 (100%). I have shown this below.

categories

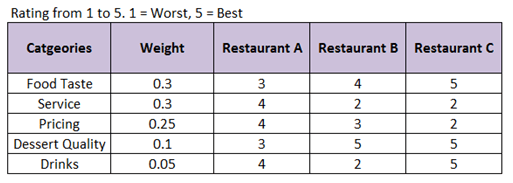
The next step is to assign the scores (1 to 5) for each category for the different options (Restaurant A, Restaurant B, and Restaurant C). This is shown below.

scores

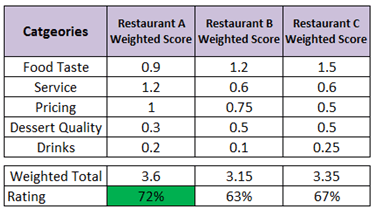
The final step is to multiply each score with its associated weighted scale, and sum it all up. This is shown below.

Pugh

This shows that Restaurant A is the best choice for me based on the initial categories I chose. This tool is applicable for all kinds of scenarios. I have attached the excel spreadsheet I used for the example here. Even in the Pugh matrix, some values carry an emotional component.

I will part with a teaching from the great Zen master Shunryu Suzuki.

“In the beginner’s mind there are many possibilities, but in the expert’s there are few.”

Always keep on learning…

In case you missed it, my last post was Talking Trash.

Talking Trash:

ごみ

In today’s post, I will be looking at how trash and waste are handled in Japan, and lessons in lean from this. There are not many public trash cans available in Japan. Yet, the cities in Japan are mostly clean. This is an interesting contrast when compared to America, where public trash cans are readily available in order to keep the streets clean.

The Lack of Trash Cans:

Japan has very limited space or land available for landfills. The main method of dealing with trash is incineration. It is estimated that about 80% of the garbage collected ends up in incinerators. In order to reduce garbage, Japanese officials in various towns and cities started implementing programs to increase recycling. This led to an interesting development. To aid recycling, the officials pushed the sorting to the source – the people. They introduced categories for sorting. Slowly the number of categories increased to double digit numbers. For example, the town of Kakimatsu in Shikoku has 44 different garbage categories. The sorting policies were strictly implemented, and those who did not comply were looked down upon. This led to public trash cans and garbage cans getting filled as part of people not wanting to sort. This may have led to the removal of several trash and garbage cans from the Japanese streets. The following is taken from the 2005 NYTimes article;

In Yokohama, after a few neighborhoods started sorting last year, some residents stopped throwing away their trash at home. Garbage bins at parks and convenience stores began filling up mysteriously with unsorted trash.

“So we stopped putting garbage bins in the parks,” said Masaki Fujihira, who oversees the promotion of trash sorting at Yokohama City’s family garbage division.

The garbage program is dealt with strictly. The peer pressure and the culture to fit in ensure that the program runs effectively. Additionally, there are “volunteers” who act as “leaders” and nudge the offenders to follow the program. It is encouraged that the trash bags are clear so that the trash is made visible. There is a cultural push to clean up after yourself and to be responsible.

Final Words:

Waste is a central theme in Lean. We are advised to eliminate waste in lean. There are many lessons that we can learn from the garbage program in Japan.

  • Everything should be based on a need- The program was put in place due to a lack of landfill space.
  • Tackle the problem at the source- The program put the responsibility at the source (the person throwing away the trash).
  • Auditing is an important aspect of any system (by your next customer or from an outside person)- For a system to sustain the auditing function is an important step.
  • Anticipate how the program can fail- the removal of public trash cans was done in response to people bringing trash from home and putting them in the public bins.
  • Any program requires people to participate in order to succeed.

As a side note, Toyota has been pursuing a zero landfill goal. As part of this, Toyota Engineering and Manufacturing of North America took away trash cans from its 1400 employees. This was described as a learning curve for the employees. The outcome of this move was that it created awareness about waste and a change in attitude.

The purging of the waste cans was a small but significant step toward Toyota’s zero-landfill goal. And Toyota has indeed achieved the goal (zero landfill is defined as diverting at least 95 percent of all waste away from landfills and into recycling or reuse).  It was one thing to reach the goal at the TEMA offices in Erlanger, where most people work at desk jobs.  Quite another to go zero landfill at its 12 manufacturing plants in North America, where they make cars, engines, auto parts and other things traditionally thought of as dirty manufacturing. Toyota has achieved that at all but two of its plants, and those  two are 97 percent of the way there. (From the article)

The other side of this is the point-of-use approach used widely elsewhere in the USA. Philadelphia is introducing a bill to require trash cans within 10 feet from the entrance of any business that sells prepared food for consumption off-premises. This is being done as a means to tackle the waste problem in the city. These seemingly two different approaches to tackle trash are interesting to say the least. The point-of-use is also an important tool used in lean to ensure that the operator has everything he needs in his reach.

I will finish off with an anecdote about Walt Disney. It is said that the average distance between two trash cans in any parks operated by Disney is 30 feet. This is based on the “study” performed by Walt Disney himself. As part of the planning he did for his parks, he ate a hot dog and he found that he took 30 steps before he was all done. He came to the conclusion that to meet the customers’ needs, he needed a trash can every 30 steps. This way the customer did not have to hold onto the trash.

Always keep on learning…

If you enjoyed this post, you can read more here.

In case you missed it, my last post was Take Pride in Your Work – Ji Kotei Kanketsu.

Take Pride in Your Work – Ji Kotei Kanketsu:

Customer

As a Quality professional, I am always interested in how “Quality” is handled in the Toyota Production System. A “Quality model” that Toyota uses is “Ji Kotei Kanketsu” or JKK. “Ji” in Japanese means “self”, “kotei” means “process” and “kanketsu” means “completion”. Putting all the words together, JKK means “Completion of your own work”. JKK has also been translated as “taking pride in what you are doing”, “not passing defects along to the next process”, or “next process is your customer”. The idea that the next process is your customer was something that Kaoru Ishikawa, the Japanese Quality Master, talked about a lot as part of the Total Quality Control movement.

Customer First:

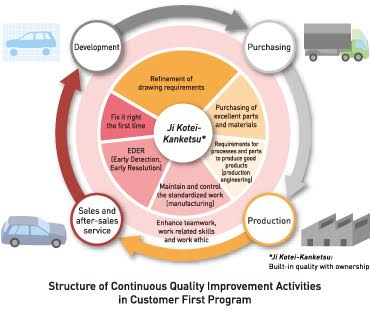
JKK was initiated by Toyota as a means to increase employee awareness about quality. Every process after your process depends on your level of quality. They are all your customers. The concept of JKK is present in all facets of Toyota. JKK starts with the Engineering group through the product design and specifications – the best possible design. This is followed by Purchasing – ensuring quality components from suppliers. This is then followed by Production – maintaining and controlling the standardized work. Finally, Sales and Marketing – early detection and resolution of any potential problems. The model below is taken from the Toyota website.

Toyota

Toyota describes the EDER (Early Detection, Early Resolution) program as follows;

EDER is a communication system for quickly detecting quality issues, immediately resolving issues, and swiftly providing results of rectification and kaizen feedback to customers.

Toyota teaches JKK as part of kaizen, continuous improvement. By focusing on your process and looking at the weak points in the process, you are identifying areas for improvement. JKK is practiced by the following four steps;

  1. First, clarify target and objective of task
  2. Clarify detailed procedure of task
  3. Clarify Ryohin jyoken (quality points)
  4. Immediately contact your supervisor, if a problem and/or delay may occur (pull Andon) and repeat Kaizen.

The Big Picture:

There is a counterintuitive aspect to JKK. By focusing on your own operation, you are required to focus on the next process – to ensure that the next process is successful. Thus, JKK is instilling a big picture mindset – a system approach in the employees.

Final Words:

The concept of Jidoka, is embedded in JKK. The ability to stop the line to fix the problem is the basis of building in quality. JKK is ensuring Quality Assurance in everybody’s work. Quality is defined as meeting customer’s requirements. Thus, customer satisfaction is the outcome of quality. In this regard, every Quality professional can be viewed as a customer service personnel.

I will finish off with an anecdote from the late founder of Matsushita Electric Industries, Konosuke Matsushita.

Matsushita was having a conversation with a western executive, and the discussion led to customers and treating customers like kings.

“No, that is wrong”, Matsushita said. “The customer is a god. Because, a king is a human, and thus capable of making mistakes. But a god does not make mistakes!”

Source: The Shift to JIT, Ichiro Majima.

Always keep on learning…

In case you missed it, my last post was Giving Time for Kaizen to Work.

Giving Time for Kaizen to Work:

time for kaizen

In today’s post I will look at kaizen and the need to allow time for an improvement to work. I am sometimes at fault about needing things to work immediately. This is a form of instant gratification – the desire to experience the results immediately. There are mainly two forms of kaizen discussed in lean literature – kaizen (small improvements) and innovation (drastic change usually involving equipment or technology). There are also medium sized improvements, and most of the time these do not result in an improvement in productivity immediately.

Shigeo Shingo and Lillian Gilbreth:

Shigeo Shingo was a consultant trainer at Toyota, and he specialized in Industrial Engineering. Shingo has written several books regarding TPS. In his book, “Key Strategies for Plant Improvement” he talked about the importance of allowing time for improvement activities to work. He referenced the “tabletop experiments” by Lillian Gilbreth as part of this. Alan Robinson along with his wife Margaret, wrote a great paper on the tabletop experiments called “On the Tabletop Improvement Experiments of Japan”. This paper talked about the contributions of Lillian Gilbreth and how her training materials were extensively used by the Japanese, and eventually by Shingo as part of his training at Toyota.

Shingo’s thinking was that the operators need to be familiar with the operation to truly feel that they are easy to do. If the steps are not familiar they have to exert their mind to think of what to do next, and this leads to mental fatigue, and thus may not result in an improvement in productivity.

Shingo discussed two experiments (Lillian had created more experiments) in his book. In the first experiment, the operator was required to write “production engineering” on 15 cards. This was a familiar phrase for the operator, and the productivity remained stable – all the cards took about the same time. The second experiment required the operator to skip every other letter, thus he was to write “poutoegneig”. The only stipulation was that he could not look at his previous work. From a work load standpoint, the number of letters were now about halved, thus it should had been a lot easier. However, the operator took a lot more time than the first experiment initially since he had to exert more time to think. After seven trials, he was able to write the word faster since he grew familiar with the phrase. The fifteenth card took about half the time as the first experiment.

Final Words:

The more I learn about Lillian Gilbreth, the more admiration I have for her. I have written about her before. The improvements may not immediately result in an increase in productivity. It is important that you understand that as part of kaizen, a certain amount of time is needed for practice to truly result in the improvement. The challenge here is – the old ways appear easier since the operator is familiar with it. Thus he may oppose the change even if it might actually reduce the work content and reduces the non-value added activities. It might be beneficial to have a standard amount of time for “sticking with the kaizen” to try it out. Rely on your data collected at the Gemba.

I will finish off with a Zen story I like a lot. This story is about how we perceive our experiences;

A student went to see his meditation teacher and said, “My situation is horrible! I feel so distracted most of the time, or my legs ache, or I’m repeatedly falling asleep. It’s terrible.” Said the teacher matter-of-factly, “It will pass.”

A week later, the student returned to his teacher. “My meditation is wonderful! I feel so ecstatically joyous and alive!” The teacher told him, “It will pass.”

Always keep on learning…

In case you missed it, my last post was PDCA and the Roads to Rome.

PDCA and the Roads to Rome:

Different roads to take, decision to make

In today’s post, I will be trying to look at the concept of equifinality in relationship to the scientific method PDCA. In Systems Theory, the concept of equifinality is defined as reaching the same end, no matter what the starting point was. This is applicable only in an open system. An open system is a system that interacts with its environment (external). This could be in the form of information, material or energy.

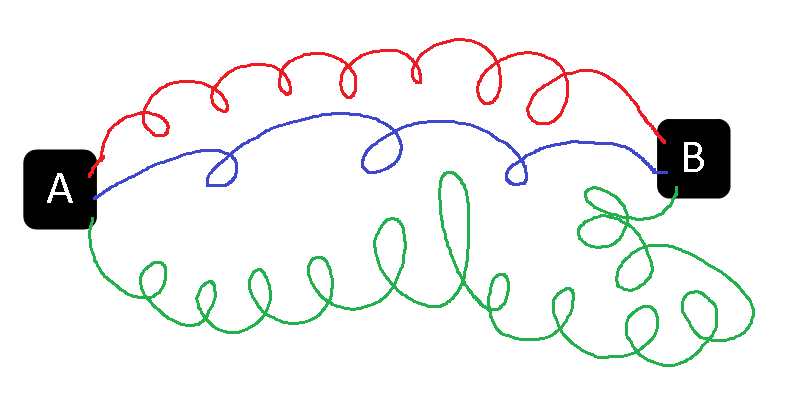
I wanted to look at the repeatability of the PDCA process. PDCA stands for the Plan-Do-Check-Act cycle, and is the framework for the scientific method. If three different people, with different ways of thinking, are facing the same problem, can all three reach the same end goal using the PDCA process? This would imply that equifinality is possible. This concept is shown below. Point A is the initial condition, and point B is the final desired condition. The three different colored lines depicts the three different thinking styles (the different thinking styles indicates the different starting points).

equi

Iterative Nature of PDCA:

The most important point about PDCA is the iterative nature of the cycle. Each cycle of PDCA leads to a new cycle that is more refined. The practitioner learns from each step of the PDCA cycle. The practitioner observes the effect of each step on the problem. Every action is an opportunity to observe the system more. The results of his experiments lead to more experiments, and yield a better understanding of multiple cause-effect chains in the system.

If the scientific method is followed properly, it is highly likely that the three different practitioners can ultimately reach the same destination. The number of iterations would vary from person to person due to different thinking styles. However, the iterative nature of the scientific method ensures that the each step corrects itself based on the feedback. This type of steering mechanism based on feedback loops is the basis of the PDCA process. This idea of multiple ways or methods to have the same final performance result is equifinality. This is akin to the saying “all roads lead to Rome”. This idea of “steering” is a fundamental concept of Cybernetics. I will be writing about this fascinating field in the future.

Final Words:

This post was inspired by the following thought – can a lean purist and a six sigma purist reach the same final answer to a problem if they pursued the iterative nature of the scientific method? There has been a lot of discussion about which method is better. The solution, in my opinion, is in being open and learning from the feedback loops from the problem at hand.

I will finish this post with a neat mathematical card trick that explains the idea of equifinality further. This trick is based on a principle called Kruskal Count.

The Effect:

The spectator is asked to shuffle the deck of cards to his heart’s content. Once the spectator is convinced that the deck is thoroughly shuffled, the magician explains the rules. The Ace is counted as 1, and all the face cards (Jack, Queen and King) are counted as 5. The number cards have the same values as the number on the card.

The spectator is asked to think of any number from 1 to 10. He is then directed to hold the cards face down, and then deal cards face up in a pile. He should deal the amount of cards equal to the number he chose in his mind. The spectator takes a note of the value of the final card dealt. The spectator is directed to deal those many cards face up on the already dealt cards.

deck_discardThis is repeated until the spectator has reached a card at which point there are not enough cards to deal. For example, the card was 8 of Hearts, and there are only six cards remaining. This card is his selected card. He then puts the face up cards on the table on top of the cards he has on his hand. They do all of this while you have your back turned. You easily find their selected card.
The Secret:

All roads lead to Rome. This trick has an over 80% success rate.

The secret is to repeat exactly what the spectator did. You also choose a random number between 1 and 10, and start dealing as described above. Just like the concept of equifinality, no matter which number you chose as your starting position, as you go through the process, you will choose the same set of cards at the end resulting in the same selected card! Try it for yourself. Here is a link to a good paper on this.

Always keep on learning…

In case you missed it, my last post was If the Learner Has Not Learned, Point at the Moon.

If the Learner Has Not Learned, Point at the Moon:

point at the moon

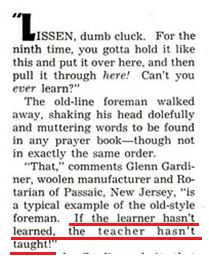
In today’s post I will be looking at the role of teaching in lean and I will try to look at the role of the student in learning. “If the learner has not learned, then the teacher has not taught.” This has come to be a common expression in Lean. This saying was introduced as part of Training Within Industry’s Job Instruction (JI) program. The original expression in the JI Program manual was “If the worker hasn’t learned, the instructor hasn’t taught.” The JI card carried the statement “If the learner hasn’t learned, the teacher hasn’t taught.”

My favorite record of this statement is from the 1942 November issue of “The Rotarian” magazine. The Albert E Wiggam’s article was titled “Foremen in 10 hours” and it talked about the Job Instruction Training program (JIT). According to the article, The purpose of the JI program was to enable the foremen to have the “show’em how” – the ability to pass the “know-how” to the new-comers in ten hours.

Rotarian

The implication in the statement “If the learner hasn’t learned…” is that the responsibility of the student’s learning rests solely with the instructor. It is my view that the student has the responsibility to be willing as well. My favorite quote regarding this comes from the most famous Japanese Samurai Miyamoto Musashi (1584 – 1645).

“Let the teacher be as a needle, the student as a thread.”

The student has to follow the teacher like a thread that follows the needle. This is a beautiful expression. The focus of the JI program is to show how to prepare the student and how to explain “the why” and “the how” of each step. It also focused on having the student repeat the operation, and to ensure that the instructor follows-up and provides the required feedback creating a closed learning loop.

 “The Ackoff Model”:

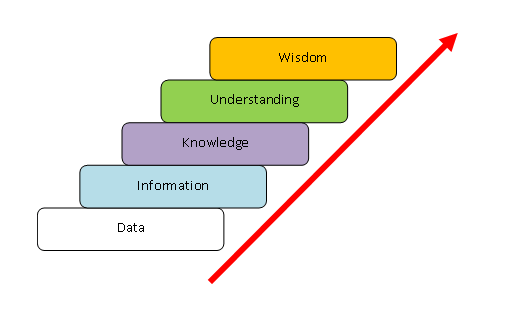
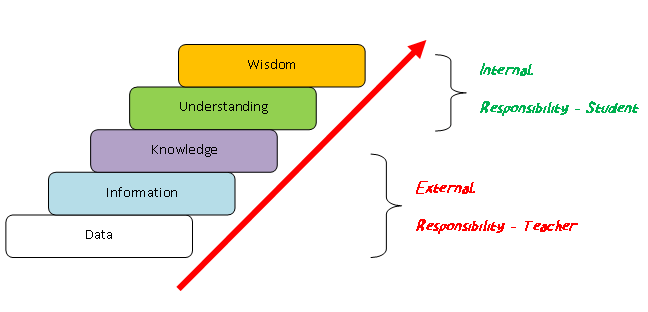
My favorite model of Knowledge Management is the DIKUW model made popular by the famous Management Science professor Russell Ackoff. This is shown below:

ackoff

The five components in the order of importance are;

  1. Data – discrete packets or values. An example for this is just a set of numbers and nouns.
  2. Information – data with context. Answers to questions such as Who, What, When, How many etc.
  3. Knowledge – answer to the question How?
  4. Understanding – answer to the question Why in a global level?
  5. Wisdom – ability to understand the situation to know what to do and execution with results

I will be using this model to further explain my thoughts. Data, information and knowledge can be imparted, and are external to the student. However, understanding and wisdom cannot be imparted and are internal to the student. The teacher can only guide the student and it is the student’s responsibility to practice and learn on his own to achieve understanding and wisdom. Perhaps, the intent of the JI is to impart knowledge to the worker on how to properly perform the operation. But the understanding and wisdom to improve one’s work (kaizen thinking) should come from the operator.

The teacher has to ensure that the student has achieved knowledge, and the student has to ensure that he achieves understanding and wisdom.

My favorite expression describing the difference between knowledge and wisdom (inspired by Peter Drucker) is;

Knowledge is doing things right and wisdom is doing the right things.

The above expression indicates that knowledge has to do with being efficient, and wisdom has to do with being effective.

The Role of the Sensei:

“Sensei” is a Japanese word that has roots in Chinese and the literal meaning in Japanese is “lives (born) before”. Sensei has come to mean “Teacher”. The term is connected with martial arts training. There are four criteria that a sensei should possess;

  1. Technical ability – understanding of the technical aspects of the subject and ability to keep on polishing/learning
  2. Taking Responsibility – ensuring that the sensei passes along his knowledge so that the “chain” does not get broken
  3. Ability to communicate – the sensei must be able to communicate his mastery to his students of all levels of aptitude
  4. Understanding – the sensei should be understanding of his students

The Role of the Student:

There is a notion in Zen that “when the student is ready, the teacher will appear”. The implication here is that the student has to be ready first and pursuing learning, only then will the teacher appear. The student can learn from everything around him only if he is receptive to learning. The student has the responsibility to present himself with humility and determination to understand and practice the skill. The student must be eager to learn and willing to “forget” what he has learned before.  My favorite account for this is an anecdote I have heard before:

A student went to a teacher and asked him “can you teach me how to meditate” and the teacher said “No. I might let you learn under me.”

 My Final Words:

It is the responsibility of the teacher to help the student attain knowledge, and it is the responsibility of the student to reach wisdom from there. Both the teacher and student have to be willing to give and receive learning. The student has to surpass the teacher. The student cannot do this simply by copying the teacher. The student has to build upon the teacher’s teachings and find wisdom on his own, leapfrogging the teacher.

teacher - student

I will finish this off with a Zen story about pointing at the moon – don’t mistake the finger for the moon.

The Buddha says “my teaching is not a dogma or a doctrine, but no doubt some people will take it as such.” The Buddha goes on to say “I must state clearly that my teaching is a method to experience reality and not reality itself, just as a finger pointing at the moon is not the moon itself. A thinking person makes use of the finger to see the moon. A person who only looks at the finger and mistakes it for the moon will never see the real moon.”

To see the moon you have to look beyond the finger.

Always keep on learning…

You may like my newer post on the cybernetic aspects of teaching and learning. If the teacher hasn’t learned, the teacher hasn’t taught.

In case you missed it, my last post was The Many Flavors of Kaizen.

The Many Flavors of Kaizen:

flavors

In today’s post I will be writing about the many flavors of kaizen. I have been writing for over a year now. It seems that I keep coming back to kaizen. Kaizen is the spirit of lean, and can be translated from Japanese as “change for the better”. What is today is not good enough, and everything can be improved in small or big steps.

There are mainly five flavors that I have identified regarding kaizen. They are;

  1. Kaizen – small incremental improvement activities
  2. Kaizen Teian – Employee Suggestion Program
  3. QC Circles
  4. Jishuken
  5. Kaizen Blitz/Event or Rapid Improvement Activity

Kaizen – Small Incremental Improvement:

Taiichi Ohno said “where there is no standard, there can be no kaizen”. His intent was that you keep improving your standard towards the ideal state. This is the essence of the Job Method program that was taught as part of the Training Within Industry program. This is where employees are encouraged to ask why a step is done in a specific manner and how an operation can be improved. Job Method program provides specific steps to do this. Ohno modified this to suit Toyota. The Job Method program was replaced by Shigeo Shingo’s P-Courses that had time and motion studies, and process and operation analysis. These courses were derived strongly from the courses taught by the Gilbreths in the early 1900’s. This type of activity is generally performed at the individual level and is thus local. These can be viewed as bottom-up kaizen.

Kaizen Teian – Employee Suggestion Program:

Eiji Toyoda went to America to learn from Ford in the 1950’s. Although he was not impressed with many things, one thing really caught his attention. This was Ford’s employee suggestion program. He brought that back to Japan and implemented it at Toyota. This really took hold in Toyota. Toyota became famous for the company with 20 million ideas in 40 years. The ideas that the employees suggest are specific to their jobs, and everybody participates in this. This type of activity is generally at the individual level and is thus local. These can be viewed as bottom-up kaizen.

QC Circles:

QC Circles are small groups of employees who voluntarily meet after work to focus on specific problems related to quality or processes. QC Circles were developed as part of the Total Quality Movement. Masao Nemoto, who is considered to be the strong force behind establishing the Quality Control program at Toyota, has indicated that the goal of QC Circles was to raise consciousness of line workers towards quality. There were a lot of improvement activities that resulted from the QC Circle activities. This type of activity is team based and generally led by a local leader like a supervisor. These can be viewed as bottom-up kaizen.

Jishuken:

Jishuken started off as a program by Toyota around 1975 for teaching suppliers how to do kaizen or implement TPS. This became a medium for training managers and other leaders in middle management. Jishuken is loosely translated as “self-study groups”. This activity generally tackles a hard project, and is seen as way to provide learning and being exposed to the gemba.  Jishuken events are also sometimes referred to as management driven kaizen activities. There is some flexibility regarding the duration of the event. There are some similarities to Kaizen events – these are team based and cross-functional in nature. These can be viewed as top-down kaizen.

Kaizen Events:

This is perhaps the most common “kaizen” identified by lean practitioners outside of Toyota. As with many things in Lean, Toyota does not practice kaizen events. This is generally a weeklong event comprising of a cross-functional team. This can be viewed as top-down kaizen.

Final Words:

It is an interesting question as to whether kaizen should be top-down or bottom-up. My thinking on this is that top management should lay the framework for kaizen to be present across the organization. The responsibility and duty for ensuring bottom-up kaizen lies with top management. Ultimately, the end goal is to get everybody to execute improvement activities so that the organization itself improves systematically. Every improvement activity should align with the organization goals and vision.I will finish off with an anecdote from Taiichi Ohno that looks at the unique relationship of top-down and bottom-up management and the need for a strong change-agent who is also a visionary.

Taiichi Ohno is the father of Toyota Production System. He first started implementing his ideas locally in his department. He faced a lot of resistance. His ideas were very counterintuitive and were against the common wisdom at that time.

Ohno was just a middle level manager. In this regard, what he did can be considered to be bottom-up. However, he had strong support from Eiji Toyoda and Saito Naichi, under whom Ohno worked for 35 years. Ohno later on talked about the positive phenomenon of the silent relationship between them in his book “Just-In-Time For Today and Tomorrow”.

There were a lot of people, including those in management who were against Ohno. However, all this anger and resentment were absorbed by Eiji and Saito. They acted as a buffer between Ohno and the factory. They never mentioned anything to Ohno. They wanted Ohno to keep on going with his improvement activities to reduce manufacturing costs. It was initially called as Ohno System since “Toyota” was not completely on board yet.  Eiji, Saito and Ohno were bound by an invisible thread of mutual trust. Ohno said the following about this;

“I knew all too well how they worried about me and what I was doing. Yet they never said “Do this!” or “Do that!”. For my part, I never had to say “I’d like to do this” or “Please let me do that.” I just did everything I thought had to be done. Had I asked permission, my resolve would have weakened because of the pressure to prove what I was doing. Had either side said anything, the relationship would have collapsed.”

Always keep on learning…

In case you missed it, my last post was Reflecting on Hansei.

Reflecting on Hansei:

hansei

In today’s post I will be looking at “Hansei”. “Hansei” is a Japanese word and has some significance in Toyota Production System. Generally I have seen this to be translated as “introspection” or “self-reflection”. I will be looking at Hansei from the Japanese culture standpoint and will try to add to the understanding of this concept.

Hansei in Japanese Culture:

The term “hansei” is related to the word “shame” in Japanese culture. However, the term does not have the undesirable emotion that we might associate with in the Western world. The term does not result in undermining oneself in the Japanese culture. The meaning speaks to making you aware that there is room for improvement and humility. There is a positive notation behind the term hansei. It is an action of criticizing oneself so that one understands the gap in their performance and thus corrects this in the future. In Japanese schools, the children are trained to perform hansei on a regular basis, generally daily. The following section is taken from the paper, “Condoned or Condemned: The Situational Affordance of Anger and Shame in the US and Japan” by Michael Boiger and Batja Mesquita;

Although shame is perceived as an unpleasant emotion in Japan, its negative valence is less pronounced than in the US (Romney, Moore, & Rusch, 1997)—possibly because it is considered conducive to self-improvement and perspective-taking (cf. Heine et al., 1999). Shame is encouraged in children: For instance, schools foster shame by the practice of hansei (critical self-reflection), a scheduled time to think about areas of self-improvement at the end of the school day (Lewis, 1995). Being aware of one’s shortcomings, and actively correcting them, affirms interdependence and helps individuals re-align with social norms and expectations.

When children do something bad, the parents say “hansei shinasai” or “do hansei”. Although this is done as part of scolding, the child is also made to realize that he can improve as an individual and this is a motivation for him to do so.

This is an opportunity for them to do the following in the correct order;

  1. Feel really sorry about what they did (recognition of what you did)
  2. Assume responsibility
  3. Understand what went wrong
  4. Correct their thinking, so that this does not repeat (desire to improve)

Through hansei we understand our shortcomings so that we can improve ourselves to be better. Kaizen (change for the better) can happen through hansei. Daily practice of hansei helps us to assume responsibility to see problems and keeps us open for improvements. Humility is one of the cherished virtues in the Eastern world. Daily hansei is an exercise to promote humility and be a life-long learner.

“Hansei Shimasu” is one of several forms of apology in the Japanese language. This is used when someone has done something pretty bad and is used to show sincere apology, deep regret and determination to not repeat the act.

In the adult life, hansei also includes an introspection of “what went right” along with “what went wrong / what could be improved”. At the end of projects, they hold “hansei-kai” – meetings to do hansei. The purpose is to learn from each other what went wrong, and what went right. These two perspectives allow an opportunity for everybody to learn. They learn from others mistakes, and they also learn from others about how to do things right – sort of a benchmarking process. There might be slightly more focus on what went wrong since they provide the real opportunity to learn.

Toyota and Hansei:

Toyota has become a learning organization and this is one of the reasons why Toyota has become so successful. Hansei has a strong role in being a learning organization. In Toyota, hansei is often viewed as a precursor to kaizen, and a pre-requisite to being a learning organization. This is best explained as below (taken from Toyota-Global website);

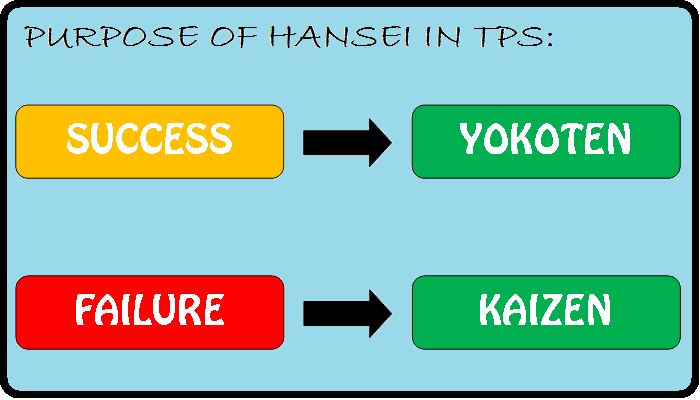
Hansei is both an intellectual and emotional introspection. The individual must recognize the gap between the current situation and the ideal, take responsibility for finding solutions, and commit to a course of action. The examination involves a review of successes and failures, to determine what works and what needs to be improved. Hansei leads to ideas for kaizen and yokoten, the sharing of best practices from one location to another.

“Yokoten” can be translated from Japanese as “horizontal deployment”. This is summarized in the graphic below:

hansei

Final Words:

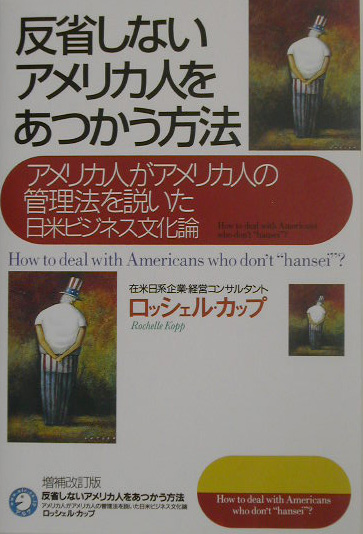
It is true that hansei forces us to look at what went wrong. However, the intent is not to place the blame, the intent is to make the person aware of the problem, and make him motivated to address the problem and not repeat it. Hansei is seen as a good thing. In the process of doing research for this article, I came across a book in Japanese titled “How to deal with Americans who don’t do hansei?” 🙂 It is an interesting title for sure!

20150830204248b22

I will finish this post with an anecdote on road rage in Japan. (Source: Asia Pacific Memo).

Psychologists working for the National Police Academy in Japan have incorporated a personal inventory test in the curriculum of the officially certified driving schools. This inventory was adapted from the Minnesota Personality Inventory, which was developed as a means to evaluate military recruits during World War I.

The purpose of this test is not to fail anybody due to their specific traits. Nobody can fail this test. The purpose of the test is to make them aware of the traits so that they can do hansei. The point is to encourage self-reflection (hansei), according to psychologists at one testing company. They believe that self-reflection among student drivers will allow them to modify their behavior or take special precautions. Those who score high on the “sensitivity” scale may be expected to adopt a zen-like attitude of tolerance and not assume that the acts of other drivers are provocations. Those who score low on the “emotional stability” scale are exhorted to focus on driving only.

There has been no evidence that this has worked. But this shows the cultural significance of hansei in Japan.

Always keep on learning…

In case you missed it, my last post was Improving the Understanding of Kaizen.

Improving the Understanding of Kaizen:

better

Kaizen is probably one of the most versatile terms in Lean. I have written several posts on kaizen. In today’s post, I will be looking at improving the understanding of kaizen. In Japanese, the word “kaizen” means to change for the better. Kaizen has come to mean several things – from “continuous improvement” to “kaizen events”. I will be sticking with the idea of change for the better.

From a philosophical standpoint, kaizen can happen two ways;

  • Problem solving kaizen – improvement through solving a problem
  • Kaizen – improvement through making things better

1 – Problem Solving Kaizen:

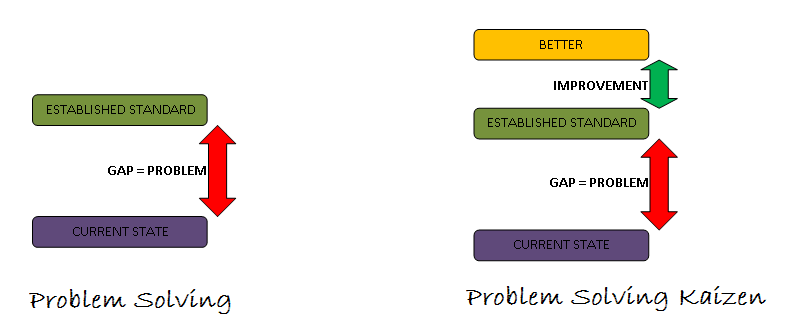
In the lean world, a problem is always defined as a deviation from the established standard. It is the gap between the current state (what it is now) and the ideal state (what it should be = established standard). As part of solving the problem, you may find a better way to surpass the established standard to a better state. This is shown below:

problemsolving kaizen

If you stop at just reaching the established standard, you may have solved the problem, but you have not made it better. Once you go higher, you have made an improvement.

2 – Kaizen – Making Things Better:

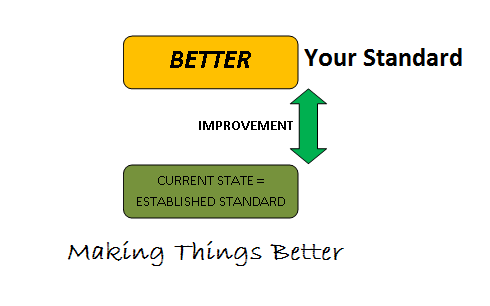
The established standard is never the best state. It is simply the state that was determined to be the acceptable standard. If we are at that level, we can expect to be performing as intended.

Making things better

Improving from the state of current standard is actually a hard task. From a production standpoint, the current state matches the established standard. However, your desired standard is higher than the established standard. This very much depends upon you and this is a hard skill to master. The extent of the kaizen depends upon the gap between the established standard and your desired standard. You can achieve this only through the belief that the current established standard is not acceptable.

This type of kaizen can be achieved by;

  1. Developing an attitude that the established standard is not acceptable.
  2. Going to the Gemba (the actual workplace). Gemba is your teacher.
  3. Understanding the current standard.
  4. Looking for waste and putting countermeasures in place.
  5. Developing others to practice steps 1 through 4.

There are several stories about Taiichi Ohno (the founder of Toyota Production System) drawing a chalk circle on the floor and asking the supervisor to stand in the circle and observe. The supervisor would stand in the circle for hours until Ohno was satisfied that the supervisor is able to see the wastes.

No task is 100% value added and free of waste. In Japanese, the term for waste is “muda”. Muda means “no value” (mu = no, da = value). Thus, muda represents non-value adding tasks. This itself has a deeper meaning. A component that is produced from a CNC machine has value. However, if the component that is produced is not needed right now by the next station, then it does not have any value. Thus, this excess inventory is identified as a form of waste in lean.

Final Words:

I have seen that the best kind of kaizen comes when you are either very lazy or very dissatisfied with something. Both of these paths lead to “there must be a better way of doing this”.

I will finish off with a story about my four year old nephew, Aaron, and how he did some problem solving on his own.

My brother has an Ipad that he allows my nephew to play games on. One day my brother and sister-in-law realized that Aaron had been watching Disney cartoons on the YouTube app. Aaron was three at the time and did not truly know how to spell words. They were surprised that he was able to find the cartoons on his own.

My brother and my sister-in-law could not figure out how Aaron was able to find the Disney cartoons on YouTube since he could not type any words to search. Aaron was not in the mood to explain how he did it either. My brother decided to watch Aaron the next time he was playing on the Ipad. Finally my brother understood what was going on. Aaron was clicking on the microphone button on the keyboard and saying the words aloud. Aaron had figured out that he could use the microphone to search. Aaron had solved the problem all by himself.

Always keep on learning…

In case you missed it, my last post was The Idea of Wa in Nemawashi.